Image
The coating looks right, the tool ships, and the delamination happens on the customer's machine.
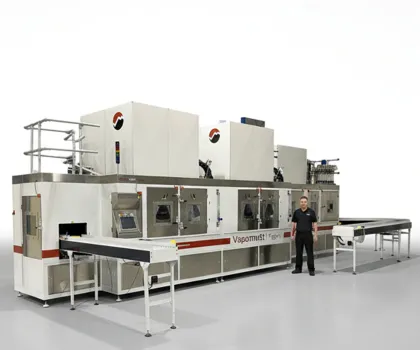
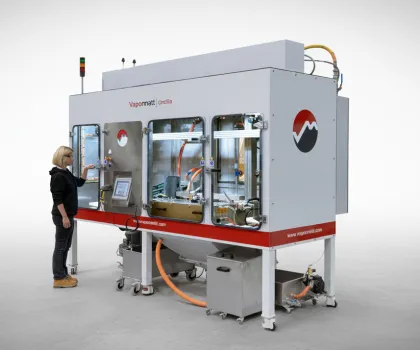
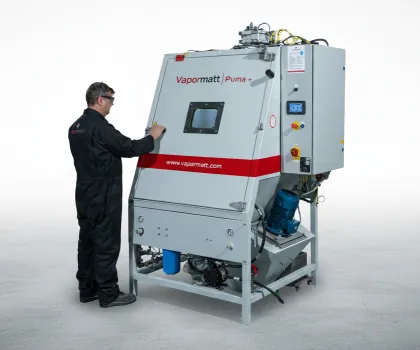
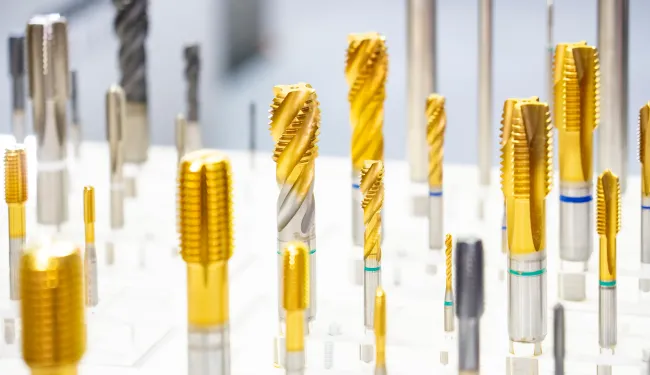
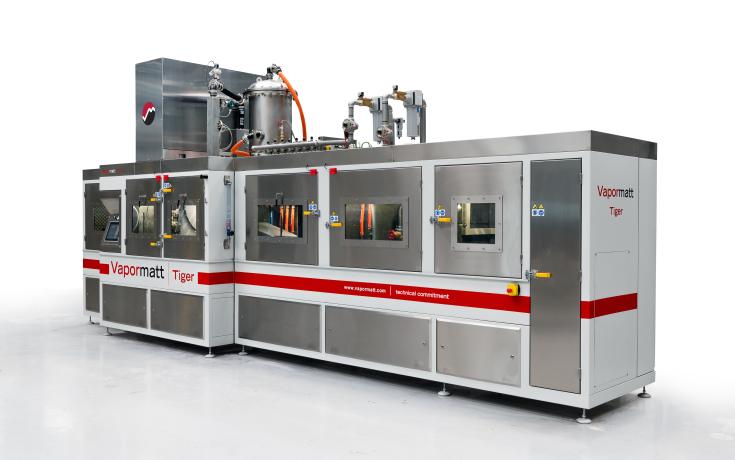
Wet blasting prepares carbide inserts and round shank tools for PVD and CVD coating by removing cobalt smear, grinding residue, sintering blisters and burrs and activating the surface, all in one controlled step. Because the abrasive is cushioned in water, it leaves no embedded media or static-charged debris, and HF1 adhesion, the top class in the VDI 3198 Rockwell C indentation test, is achievable. Every process variable is locked and logged, so the surface going into the coater is consistent across the batch, not just the sample. The same process prepares reground tools for recoating.
Talk to an applications engineer about your coating prep requirements
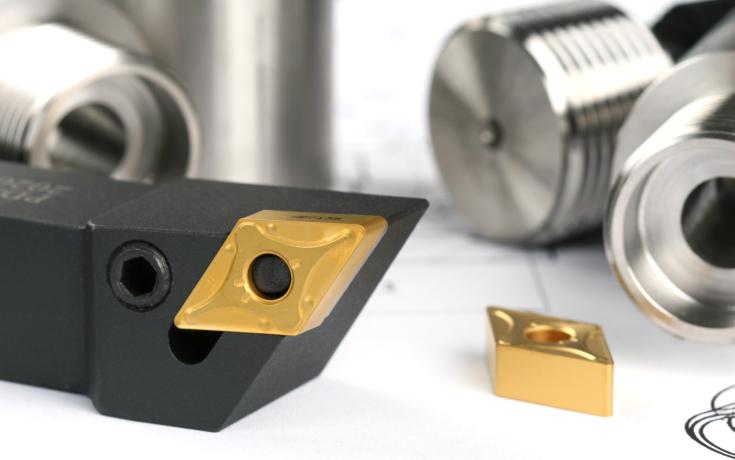
The slurry stream carries fine abrasive particles in a water cushion that cleans and activates the substrate without introducing the micro-cracking that dry processes can cause. Pressure, abrasive concentration, and gun geometry are held within tight tolerances, so the surface condition delivered to the coater is defined and repeatable rather than operator-dependent. For PVD and CVD applications, where coating adhesion is sensitive to nanoscale contamination and surface energy, that repeatability is the difference between a coating that bonds and one that does not. On solid carbide tools, pre-coat activation and edge honing can run as a single operation with fine media, removing a process step.
Typical setup: PVD/CVD coating preparation
The parameters below are confirmed for the component types listed. All figures are indicative ranges; exact parameters are set during application development for your specific substrate and coating system.
| Component type | Typical size or weight | Process mode | Achievable outcome | Minimum control |
|---|---|---|---|---|
| Cutting inserts | ~15 x 15 x 8 mm | Automatic (radial or X-Y) | Cobalt smear and grinding residue removed; can be combined with edge honing; HF1 adhesion achievable for excellent PVD / CVD bonding and subsequent extended tool life | Automatic motion, air pressure control |
| Round shank tools (RSTs): drills, end mills, taps | ~Ø15 mm x 70 mm | Automatic (vertical) |
"Wet blasting is the preferred surface finishing option for coating specialists."
PVD and CVD coatings bond at the atomic level and are applied under high temperature and vacuum conditions. Any contamination or surface inconsistency on the substrate at that point becomes a failure site. The coating may pass visual inspection and still delaminate under load because the adhesion was never fully established. Getting the substrate right before the tool reaches the coater is the only point in the process where that risk can be removed.
Automatic motion control and closed-loop air pressure control remove the two biggest sources of batch variation. Abrasive type and mesh, pressure, gun configuration, motion path and cycle time are set, locked and logged, so every part gets the same treatment and the preparation step can be documented like any other controlled stage. If a batch falls outside tolerance, the records show where and why. Talk to an applications engineer about documenting the process for your quality system.
Yes, but not in the same machine cycle. Inserts and RSTs require different gun configurations: crown geometry for inserts, vertical oscillation with satellite drive for RSTs. Production lines running both component types route them through separate dedicated setups or a machine specified to switch between configurations.
For carbide cutting tools, yes. Dry blasting leaves a rougher surface and can embed media: in Platit’s 2019 Edge Pre-treatment Compendium, wet-blasted carbide measured Sa 0.05 µm against Sa 0.11 µm for dry blasting. Brushing leaves the cobalt binder in place, which weakens the coating interface. Wet blasting removes it, exposing the carbide grain for the coating to bond to.
See the full comparison of dry blasting, brushing and wet blasting
Fine aluminium oxide at 320 to 500 mesh is the standard abrasive for this application. The mesh size matters because it controls the energy delivered to the surface at a microscopic level. Too coarse and you risk altering the substrate in ways that affect coating uniformity; too fine and the activation effect is insufficient. Aluminium oxide at this range cleans and activates without compromising the substrate, and it performs consistently across carbide and other common cutting tool materials.
Yes. After PVD coating it removes the droplets left on the surface, lowering roughness and friction. After CVD coating it converts tensile stress in the coating to compressive stress, which reduces flaking in use.