Image

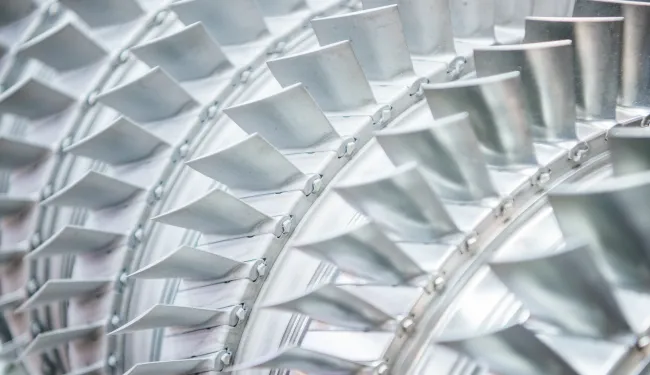
A blade that fails fatigue inspection means a grounded engine, a halted production line, and a rework bill that dwarfs the cost of the process that caused it.
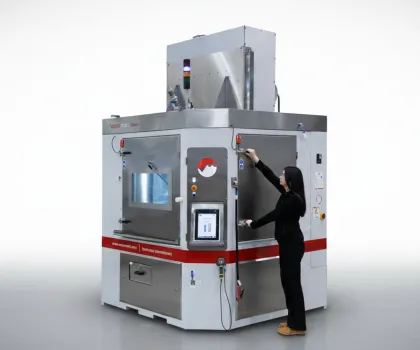
Wet shot peening (also called wet peening) is a cold-working process in which spherical media, carried in a water slurry, is propelled at a component to induce compressive residual stress, extending fatigue life and resisting crack initiation. The water flushes debris away continuously, so the peened surface is clean and free from the contamination dry processes leave behind. Every variable (air pressure, media concentration, gun position and motion) is monitored in closed loop, and Vapormatt automatic machines comply with AMS 2432, so the intensity your engineer specifies is the intensity the machine holds, cycle after cycle.
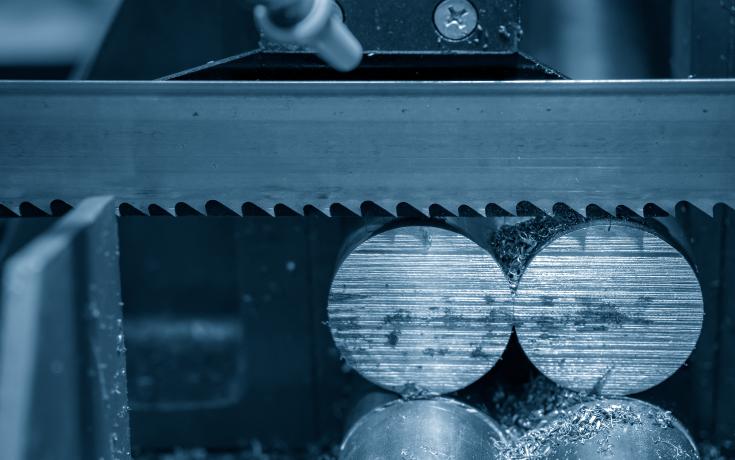
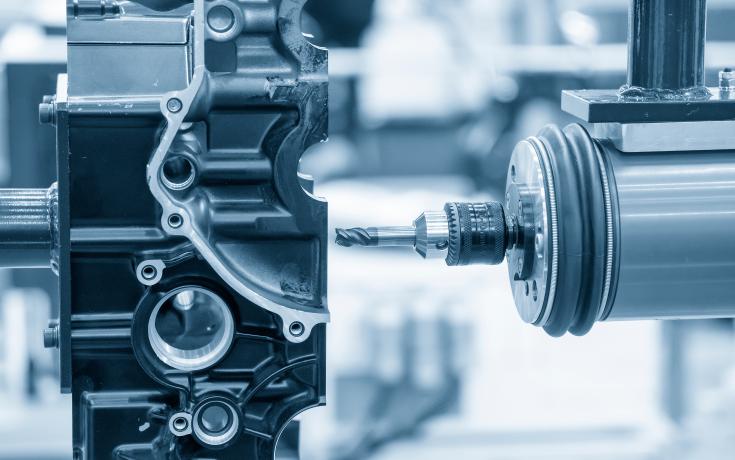
A slurry of spherical media suspended in water is propelled at the component surface under controlled air pressure. The media imparts compressive stress at the point of impact; the water film prevents media fracture, controls the energy delivered per impact, and carries away contaminants without embedding them. Adjusting air pressure, media type and size, gun geometry, and component motion changes the peening intensity achieved, giving engineers a precise and repeatable lever for each component specification.
Typical setup: peening
The parameters shown below are indicative and confirmed for the component types listed. Wet shot peening handles the full range from precision aerofoil surfaces to continuous industrial tooling.
| Component type | Typical size or weight | Process mode | Achievable outcome | Minimum control |
|---|---|---|---|---|
| Aerospace titanium fan blade (Ti-6Al-4V aerofoil) | Up to approx. 1.5 m span | Automatic — turntable with Z-axis oscillation | Almen intensity 15–20N (Type N), 200% coverage | Closed-loop air pressure control; automatic motion |
| Aerospace LPC blade (titanium alloy, multi-stage) | Small aerofoil, multi-stage variants | Automatic — turntable with Z-axis oscillation | Almen intensity 7–13N (Type N), 100% coverage, intensity window held across 13 measurement positions | Closed-loop air pressure control; automatic motion |
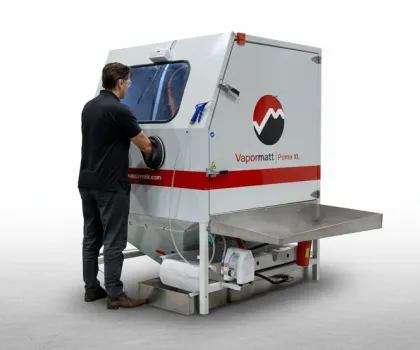
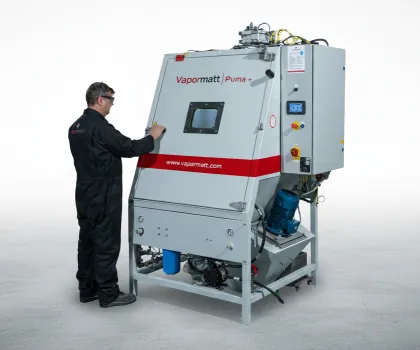
| 3D printed tensile test sample (aluminium alloy) | Approx. 200 mm x 10 mm x 8 mm | Manual | Compressive residual stresses created | Basic manual machine |
| Bandsaw blade (continuous, industrial) | 70 mm height, continuous coil | Automatic — continuous (Profelis) | 1500 MPa compressive residual stress | Closed-loop air pressure control |
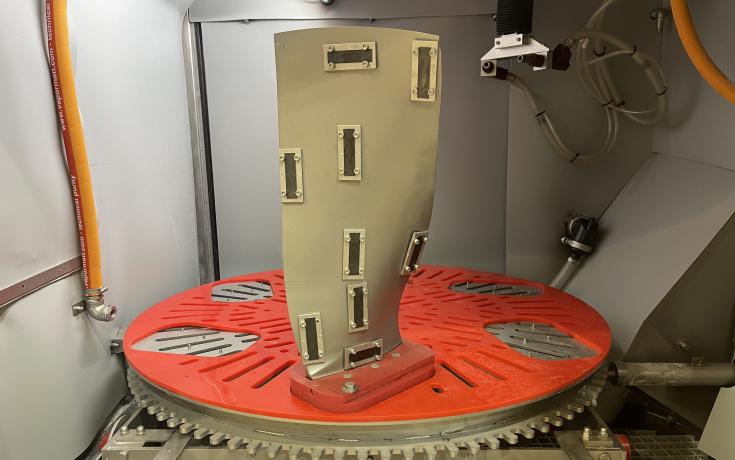
A Japanese aerospace manufacturer needed to validate wet shot peening against customer-specified Almen intensity windows for titanium fan blades and multi-stage LPC blades, with 13 Almen strip positions on the fan blade and separate saturation curves required for each blade stage. In Vapormatt sample processing trials using a Sabre wet blasting machine configured to replicate a Cougar+ Vertical, with glass beads size No.5 at 5–6 bar air pressure and 2.4 bar slurry pressure, all 13 fan blade positions returned intensities within the 15–20N window, and LPC blade stages met their respective 7–11N and 10–13N specifications. Source: Vapormatt sample processing trial TRF-1884.
Wet shot peening is used across aerospace, cutting tools and additive manufacturing. For OEM and MRO requirements on fan blades, discs and blisks, see jet engine peening; for continuous product, see bandsaw blades; for printed parts, see additive manufacturing.
Vapormatt co-authored the first technical paper on wet shot peening with 'The Shot Peener'
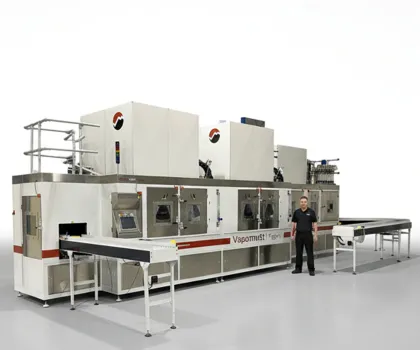
Profelis - continuous product such as bandsaw blade up to 100 mm high, peened in-line on a multi-gun gantry where throughput per metre is the primary commercial driver.
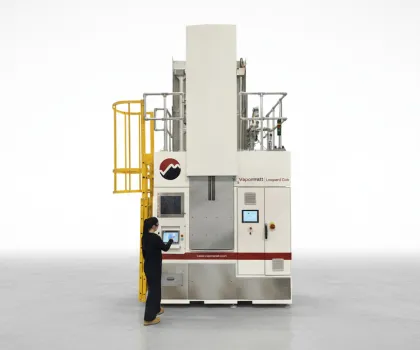
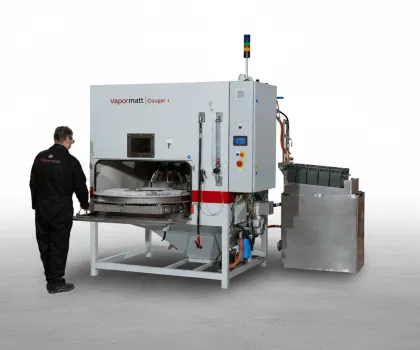
Cougar+ - medium to large discrete components, including aerofoils up to approximately 1.5 m in the vertical configuration, where long production runs and closed-loop process control are both required.
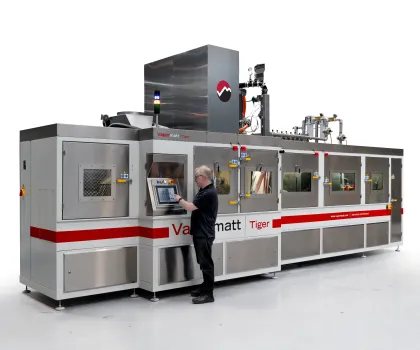
Sabre - high-value components with complex geometries, where five-axis CNC control is needed to hold intensity and coverage on every surface, and the machine used for the titanium fan and LPC blade trials above.
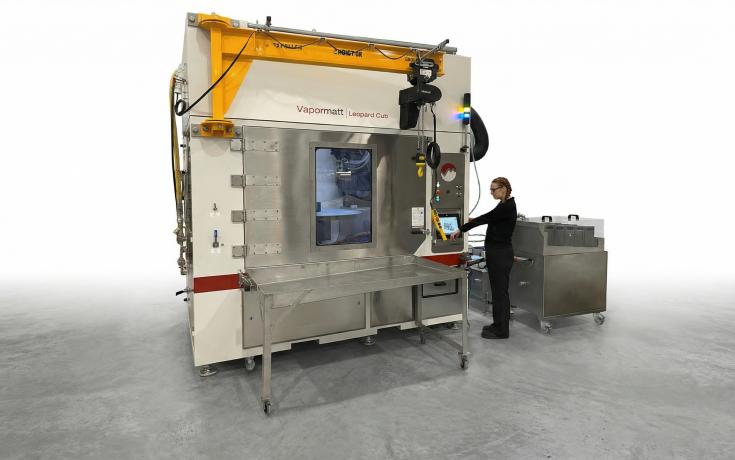
Leopard Cub - AMS 2432 compliant aerospace peening for MRO teams whose components don’t need the full Leopard envelope.
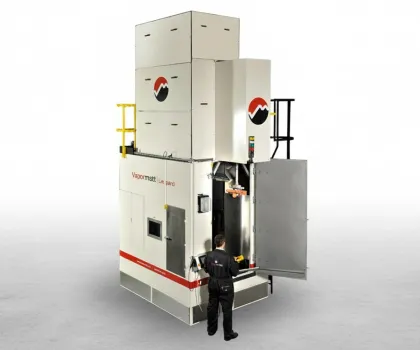
Leopard - large-format aerospace MRO and OEM peening of safety-critical components, with AMS 2432 process control and full cycle logging.
Wet shot peening carries the media in a water slurry instead of an air stream. It reaches the same Almen intensities as dry peening, up to [39N / 38A], but the water stops the media fracturing, so impact energy stays consistent and the finish is smoother. There is no airborne dust, so titanium and other reactive alloys don’t need ATEX-rated extraction. Oil and grease on incoming parts are removed during the cycle, which removes the separate pre-cleaning step that dry peening specifications require.
Validation uses the same Almen method as dry peening. Type N or Type A strips are placed at multiple positions on the component, and a saturation curve is plotted by doubling exposure time at each step until arc height rises by 10% or less. Once saturation is confirmed, the recipe is locked and held in closed loop, and the results are documented in a test report. If your specification has several intensity windows on one part, each section is validated separately. If it names a media standard, such as CSS 8 VG300 AECMA prEN 2750 for glass beads, conforming media is used.
Yes, provided the blast stream stays perpendicular to the surface as the component moves. Vapormatt machines do this with multi-axis component manipulation: a turntable with Z-axis oscillation for most aerofoil work, and robotic positioning for the most complex geometries. In Vapormatt trials on titanium fan blades (TRF-1884), all 13 Almen strip positions on a single blade fell within the specified 15–20N window.
Yes. Each component type has its own stored recipe covering media, pressure, gun position and motion profile, so changing between parts means selecting a recipe, not setting the machine up from scratch. In mixed production, fixturing matters more than recipe changeover: if components share a fixture family, changeover time is minimal.
No. The water is a cushion and carrier, not a reactant. It prevents media fracture, which keeps media geometry consistent and avoids the angular debris that can contaminate surfaces in dry processes. A DI water rinse removes residual media and slurry after peening, so the surface leaves the machine clean and ready for inspection or coating without an extra cleaning stage.