

Every cutting tool earns its reputation at the edge. Whether you make solid carbide drills, indexable inserts or bandsaw blades, or you regrind tools, the edge decides your reject rate, your coating performance and whether your customer reorders.
Wet blasting controls that edge with more consistency than brushing, drag finishing or dry blasting. Our machines hone edge radii from 5 to 70µm with patented K-factor control (GB2590936B). They hold ±5µm on inserts and as tight as ±2µm on solid round tools, and leave a clean, reactive surface for PVD or CVD coating.
No single machine suits every cutting tool. Inserts, solid round tools, bandsaw blades and files each need a different way of holding the part, a different level of automation and a different throughput, so each machine below is built for a specific tool type and volume. Before you commit, we process your own tools at our R&D facility in Bridgwater, UK, and return them with measured edge radius and K-factor data.
Compare our machines for cutting tools

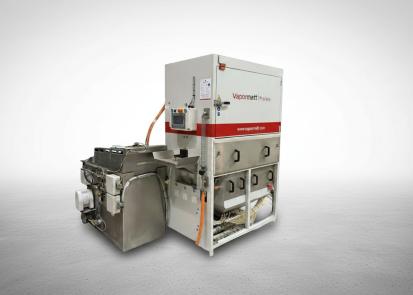
Puma+
Compact with four configurations, suited to smaller component runs, solid tools, and factories that need consistent automated processing.

Oncilla
End-to-end automated cell for solid carbide round shank tools, integrating cleaning, K-factor edge honing and coating preparation in one cycle.

Cougar+
Robust and highly configurable with 32 options. Built for long production runs across demanding applications, from aerospace peening and cleaning to extrusion die maintenance.

Tiger
High-volume in-line machine for carbide insert edge preparation, cleaning, peening and coating preparation, with integrated washing and drying as standard.

Tiger+
Dual chamber combined insert edge preparation and coating preparation, with washing and drying, integrated into a single and continuous production line.

Jaguar
High-capacity carbide insert finishing: six pallets per cycle, edge radii held to ±5µm, with an optional shuttle for loading during production.

Profelis
The only purpose-built inline wet blasting machine for continuous wire, cable, strip and bandsaw blades, from 1mm (0.04") to 54mm (2.13").

Sabre
Five-axis CNC precision cell for high-value components with complex geometries, where conventional automatic blasting cannot deliver the required control.
Profelis FR
Cleans heat scale and quench residue from files and rasps and sharpens the cutting edge in a single conveyor pass, then rinses and dries each file with a clean, even finish.
Which machine do I need for my cutting tools?
Choose by tool type first, then by weekly volume and how many finishing stages you want in one machine.
| Machine | Tool type | Volume | What it does | Edge hone |
|---|---|---|---|---|
| Tiger | Indexable carbide inserts | Very high, continuous in-line | Edge honing, pre-coat cleaning, post-coat peening and polishing, rinse and hot-air dry | ±5µm |
| Tiger+ | Indexable carbide inserts | Highest: two blast chambers | As Tiger, plus honing and polishing in a single pass | ±5µm |
| Jaguar | Indexable carbide inserts | High, batch: six pallets per cycle | Edge honing, deburring, pre- and post-coating treatment | ±5µm |
| Sabre | Inserts, round shank tools, or both (hybrid) | Small to medium; coating centres and R&D | Five-axis CNC edge honing and coating preparation | ±5µm |
| Oncilla and Oncilla Cub | Solid carbide drills, end mills, taps, thread mills | Over 2,000 tools per 24 hours (Oncilla); low to medium (Cub) | Cleaning, K-factor edge honing and PVD preparation in one cycle | 2–30µm radii, ±3µm |
| Puma+ (Vertical with satellites) | Round shank tools, 3–25.4mm diameter | Low to medium batches, 42 tools per load | Batch edge honing, cleaning and coating preparation | Set to your specification |
| Cougar+ | Inserts and other cutting tools | Long production runs | Configurable cleaning, honing and finishing | Set to your specification |
| Profelis | Bandsaw blades | In-line, at line speed | Tooth honing, gullet peening, cleaning for coating | 5–50µm radii |
| Profelis FR | Files and rasps | Around 500 files an hour (200mm file) | Heat scale removal and tooth sharpening | Not applicable (sharpening) |
Not sure which fits? Send us your tools, target edge radius and K-factor, coating system and weekly volumes, and an applications engineer will recommend a machine and configuration with an indicative budget.
Why cutting tool manufacturers choose Vapormatt
- We built the first automated edge honing machines for cutting tool inserts in the 1980s, and co-developed insert finishing technology with Sandvik.
- We hold the patent for K-factor edge control by wet blasting (GB2590936B), so the hone is controlled across the rake and clearance faces, not just the radius.
- In production, an Oncilla holds a 10–15µm edge hone to Six Sigma, delivering up to a 50% improvement in cutting performance.
- A Sabre runs at Ionbond’s coating demonstration centre, preparing tools for coating.
- Every machine is factory acceptance tested, often on your own tools, and backed by the Vapormatt Promise: it meets the agreed specification, or we make it right.
- We have supplied more than 2,000 machines to over 50 countries since 1978, with local support through our global partners.
FAQs
Which machine is right for carbide inserts: Tiger, Tiger+, Jaguar, Sabre or Cougar+?
It depends on your volume and how many finishing stages you want in one machine. Choose the Tiger for very high-volume, unattended in-line production with washing and drying built in. Choose the Tiger+ when you need double that output, or edge honing and polishing in a single pass. Choose the Jaguar for high-capacity batch processing of six pallets per cycle, with washing and drying done separately. Choose the Sabre for small to medium volumes, coating centres and R&D, and the Cougar+ for long production runs on a highly configurable machine. The Tiger, Tiger+, Jaguar and Sabre all hold edge radii to ±5µm.
Which machine is right for solid carbide drills, end mills and taps?
For high volumes, choose the Oncilla. It is a robotic cell that cleans, K-factor edge hones and prepares solid carbide drills, end mills, taps and thread mills for PVD coating in one cycle, at over 2,000 tools per 24 hours, with radii from 2 to 30µm. The Oncilla Cub brings the same process to low-to-medium volumes. For smaller batches, the Puma+ Vertical with satellites processes 42 tools per load, from 3 to 25.4mm in diameter.
Can one machine process both inserts and round shank tools?
Yes. The Sabre hybrid configuration has ten blast guns, eight for inserts and two for round shank tools, under five-axis CNC control, so one machine can edge hone and coating-prep both. It suits small to medium volumes, coating centres and R&D facilities. For high volumes of one tool type, a dedicated machine gives more throughput: the Tiger for inserts or the Oncilla for round tools.
How much does an edge honing machine for cutting tools cost?
The price depends on throughput, the level of automation, how tools are loaded and held, and whether washing, drying, an elutriation tower and process data logging are included. We give you an indicative budget and running costs at the first recommendation stage, so you can build your business case before you ask for a formal quotation.
What do you need from us to recommend a machine?
Send us drawings or details of your tools, the tool type and substrate, your target edge radius and K-factor, the coating system you use and your weekly volumes. An applications engineer will recommend a machine and configuration and give you an indicative budget.