

Discuss you deburring requirements with a process engineer
Removing a burr is easy. Removing it without changing the edge you machined so precisely is the hard part.
Wet blasting (also known as vapor blasting) removes category 1 and 2 micro and feather burrs from machined parts, cutting tools and surgical instruments, cleaning and degreasing them in the same pass, without changing critical edge geometry. Burrs left on these parts are not cosmetic. On tooling, they concentrate heat at the cutting edge, accelerate wear, and cause coating adhesion to fail at exactly the point where it matters most. On surgical instruments, category 1 and 2 burrs present a patient safety risk that no downstream inspection process can fully mitigate.
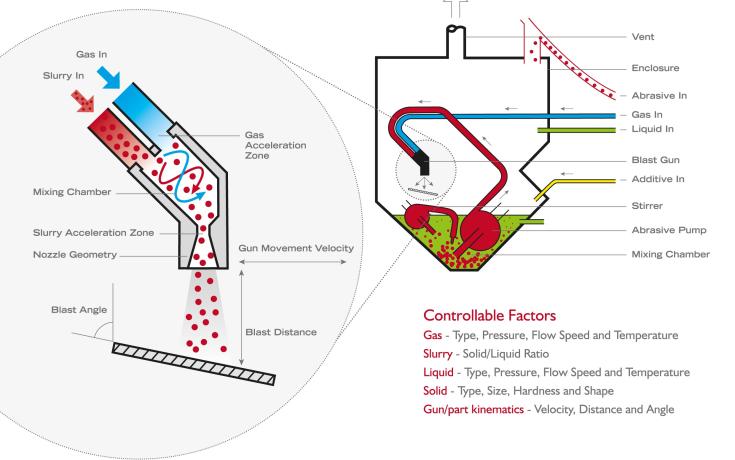
How wet blasting deburring works in practice
The slurry cushions the abrasive in water before it reaches the surface. This reduces the peak impact energy of each particle, which is why the process removes category 1 and 2 burrs without loading the base material or significantly changing the edge radius. In addition the water flows the abrasive around hidden corners. Pressure, abrasive type, gun angle, and component motion are each independently adjustable, which means the recipe can be dialled to the burr size and substrate without trading off one outcome against another.
Typical setup: deburring
- Abrasive: Aluminium oxide, typically around 220 mesh; glass bead for softer substrates or where a bright finish is required
- Pressure: 4 to 5 bar (58 to 73 psi); lower for soft metals or where edge radius change must be minimised
- Guns: Manual or automatic depending on component; automatic motion required for repeatable results on cutting tools
- Minimum recommended control: Basic manual machine for general machined parts; automatic motion control for cutting tools and precision instruments
- Variables: Edge radius tolerance drives acceptable aggressiveness; geometry complexity and internal cavities require gun angle and standoff adjustment
Deburring capability: what wet blasting achieves
The process handles the component types shown below. Parameters shown are indicative and confirmed for the component types listed.
| Component type | Typical size or weight | Process mode | Achievable outcome | Minimum control |
|---|---|---|---|---|
| HSS taps (M8, flute deburring) | 8mm diameter | Semi-automatic | Category 1 and 2 burrs removed; edge radius affected very slightly | Automatic motion |
| Brass water valve parts (multi-geometry fittings) | Approx. 80 x 75 x 60mm | Manual | Good burr removal across internal cavities and machined faces; surface finish affected slightly | Basic manual machine |
| Titanium surgical tips (three tip geometries) | Approx. Ø15mm x 150mm | Automatic | Effective deburring with micro-geometry kept intact; met visual deburring standard | Automatic motion |
In Vapormatt sample processing trials, 8mm HSS taps from a European cutting tool manufacturer were processed to remove category 1 and 2 burrs along the flute with minimal change to cutting edge geometry. A Vapormate set up to replicate the automatic motion of an Oncilla production machine was used with Expo-blend abrasive and a custom deburring gun at 2.5 bar. Burrs were fully removed in 5 seconds per tap, with average edge radius results of 16.31, 19.91 and 16.79 µm across tested tools, confirmed by Alicona EdgeMaster measurement.
Buyers processing surgical or dental instruments will find relevant context on the medical and dental instruments page. Manufacturers processing cutting tools should also review the cutting tool inserts and solid carbide tools pages before specifying a machine.
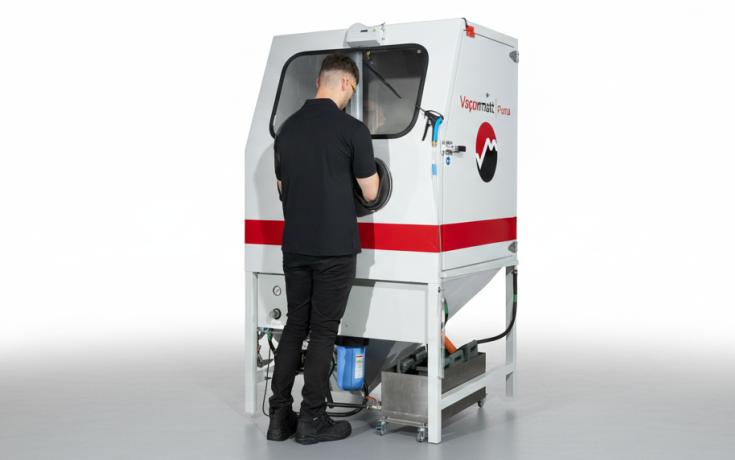
The right machine for your application
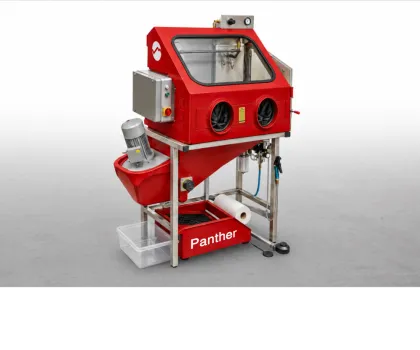
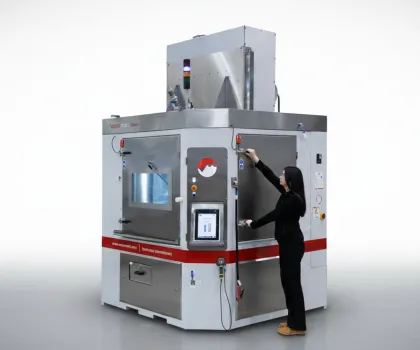
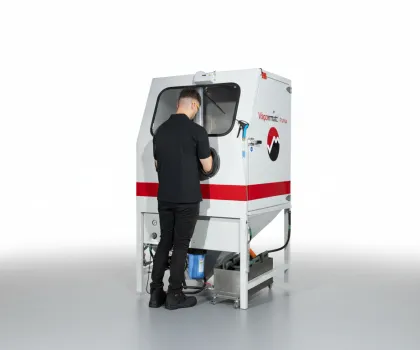
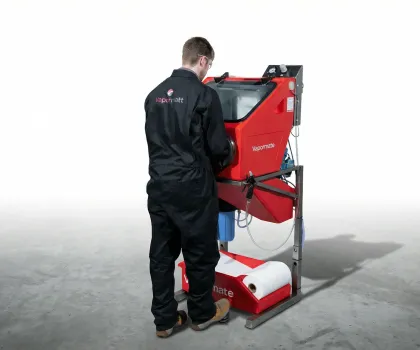
Vapormate or Puma: the right starting point for a wide range of component types with low to moderate throughput requirements and basic control specification.
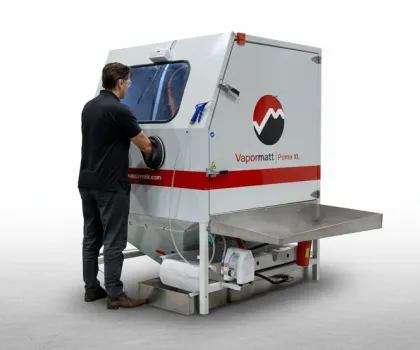
Puma XL: for large components that exceed the envelope of a standard machine.
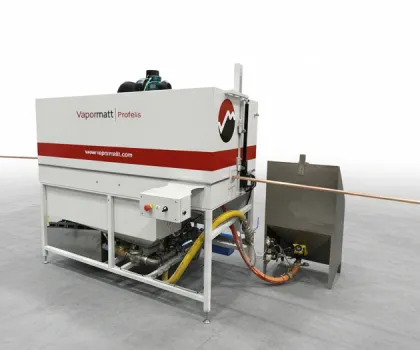
Puma with barrel: for small parts requiring high throughput where individual component handling is not practical.
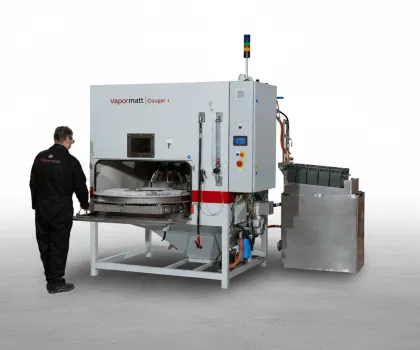
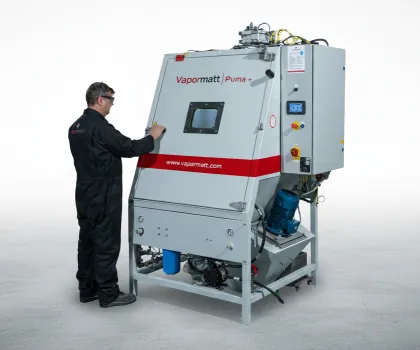
Puma+: for repeatable automatic deburring of smaller components and solid tools.
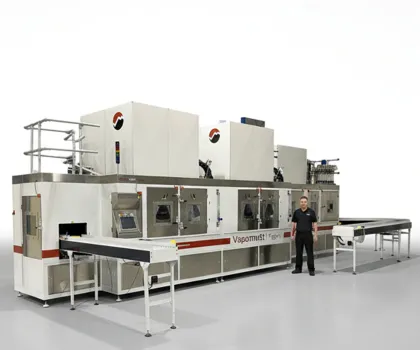
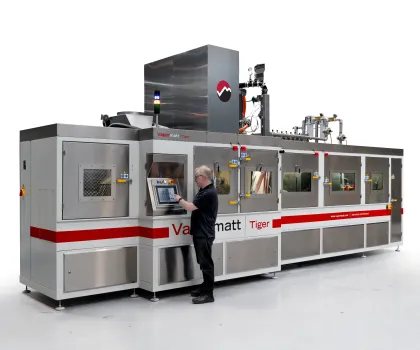
Oncilla: robotic cell for taps and other round shank tools, and precision instruments that need automatic motion to hold edge geometry from part to part.
Related machines
FAQs
What size of burr can wet blasting remove?
Wet blasting removes category 1 and 2 burrs: the micro and feather burrs produced by machining. Categories 3 to 5 are progressively larger and stiffer; at those sizes, the process may not remove the burr without a surface change that falls outside acceptable limits. A process engineer can confirm whether your specific burr falls within range.
How does wet blasting compare with vibratory, brush and manual deburring?
Wet blasting gives more control than vibratory, brush or manual deburring, and reaches complex geometry and internal features those methods struggle with. Vibratory and tumble finishing suit bulk deburring of robust parts but give little control over individual components; brush finishing works on flat and rotary parts but is limited on complex 3D shapes; and manual deburring depends on operator skill. Wet blasting also cleans and degreases the part in the same pass.
Which materials can be deburred by wet blasting?
Wet blasting (also known as vapor blasting) deburrs both hard and soft metals, including HSS, tungsten carbide, titanium, stainless steel and brass. Aluminium oxide is typically used on harder materials, while glass bead suits softer substrates or where a bright finish is required. Pressure is reduced on soft metals to protect edge radius and surface finish.
Will wet blasting open the edge radius on my cutting tools?
It can, which is why pressure and abrasive selection matter. In sample processing trials on 8mm HSS taps, average edge radius values after processing ranged from 16 to 20 microns with a custom deburring gun at 2.5 bar. The recipe is set by adjusting pressure and abrasive aggressiveness against your edge radius tolerance, not by applying a standard programme. If you need a defined edge radius rather than to preserve the existing one, see edge honing.
Can the process reach burrs in internal cavities and cross-holes?
Yes, for accessible cavities. In trials on brass water valve parts with internal machined geometry, blasting into inner cavities removed the majority of accessible burrs cleanly. Burrs in geometry that physically prevents gun access cannot be reached by any blast process; these cases are identified before a machine is specified.
How long does wet blasting deburring take?
Cycle time depends on burr size, component geometry and how the parts are handled. As a benchmark, in Vapormatt trials burrs were fully removed from the flutes of 8mm HSS taps in 5 seconds per tap. Barrel processing handles batches of small parts together, and automatic machines repeat the same cycle time on every part.
How do I know the process will be consistent enough for a medical application?
Consistency is a function of how well the recipe is controlled and how repeatable the component motion is. For titanium surgical tips, automatic motion on the Oncilla allowed the same programme to process multiple tip geometries to a confirmed visual deburring standard. The process can be locked and documented so that every part receives the same treatment.
Do I need a high-specification machine to deburr general machined parts?
Not for straightforward applications. Brass fittings and similar components were processed effectively on a basic manual machine. The level of control required scales with the tightness of your edge radius or surface finish specification, not with part complexity alone. A process engineer can tell you which level your parts need.