Image
Don't let your peening process be the weakest link in your quality chain
Selecting the wrong wet peening equipment supplier means running a process that is technically compliant on paper and non-conforming in production. For rotating engine components processed to OEM specifications, the margin for process drift is zero. Every cycle must be traceable, every Almen strip result within tolerance, every parameter logged and auditable.
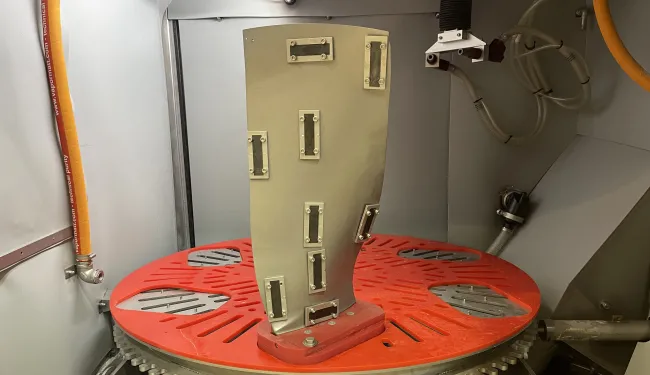
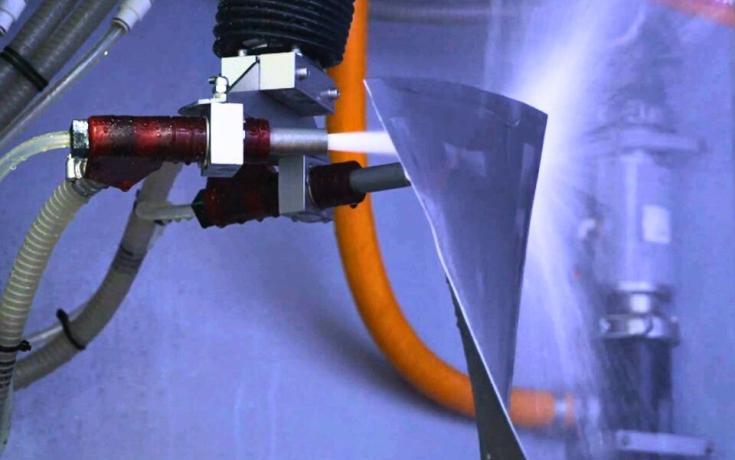
Wet shot peening fires ceramic or stainless-steel shot, carried in water, at a component to induce compressive residual stress and extend fatigue life. Vapormatt’s AMS 2432 compliant machines peen fan, compressor and turbine blades, blisks and discs for OEM manufacture and MRO overhaul, including work to Rolls-Royce, GE and Pratt & Whitney specifications. Below are our credentials and the five reasons engine manufacturers choose us.
Peens to the same intensity as dry shot peening
Produces a higher quality surface finish than dry shot peening
More controllable than any other peening process
Produces the same uniform results every time
Vapormatt has been designing and supplying wet peening machines for jet engine components since the 1980s. Wet blasting itself was developed in the late 1940s by Norman Ashworth, working with Sir Frank Whittle on jet engine development. That depth of understanding, built across four generations of the founding family, distinguishes our application knowledge from every other supplier in this market.
In the early 1990s, Vapormatt’s G. Wallis wrote “Peening and Wet Peening” for The Shot Peener (Vol. 5, Issue 1), the first technical paper on wet shot peening, establishing the process and equipment framework the aerospace sector subsequently adopted.
Download the 'Peening and Wet Peening, The Shot Peener Vol.5 Issue 1' article
Our automatic wet peening machines comply with AMS 2432 (Shot Peening, Computer Monitored) and our installed base includes MRO operations processing components to Rolls-Royce, GE, and Pratt and Whitney specifications.
Read our aerospace industry MRO brochure
Read our aerospace industry OEM brochure
The fundamental challenge in wet shot peening is one that generic wet blast equipment is not designed to solve. Peening media, ceramic or stainless-steel shot, is significantly denser than blasting abrasives. At operational concentrations it settles rapidly, stratifies in feed lines, and pulses at the nozzle. The result is inconsistent slurry concentration, variable impact energy, and Almen intensity readings that drift across a batch.
Vapormatt addresses this through high-powered vortex pumps engineered specifically for dense media, patented non-blocking elutriation towers, and inline concentration measurement that monitors and adjusts slurry consistency throughout the cycle. The Rolls-Royce RPS428 specification requires bead-to-water ratio to be maintained to a maximum of 45% by volume. Vapormatt systems hold that ratio within declared limits continuously, with shot flow, air pressure, nozzle position, and cycle time all monitored in real time with automatic shutdown on deviation.
In a trial for a Japanese aerospace manufacturer, all 13 fan blade Almen positions fell within the specified 0.15-0.20 mm N window, and every LPC stage met its own specification. See the trial results.
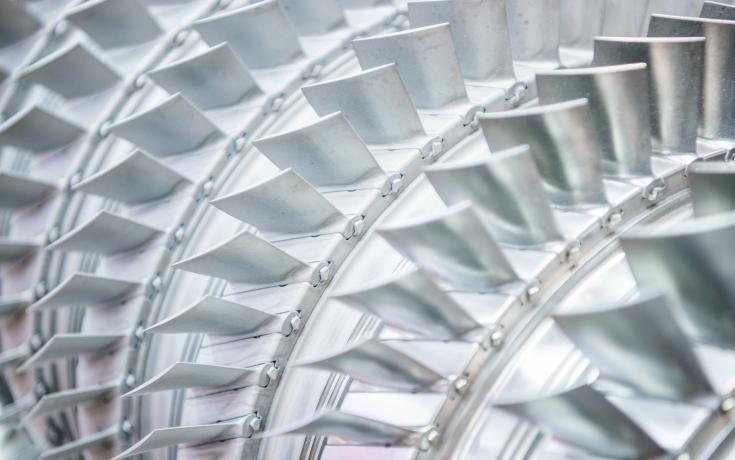
Vapormatt systems peen the full range of rotating and structural engine components across OEM manufacture and MRO overhaul:
Peening a component not listed here? Send us the drawing and governing specification, and our applications engineers will recommend a process.
Internal and complex geometry peening. Disc fir-tree slots, blade root bores, and other confined features present a coverage challenge that conventional wet nozzles cannot reliably solve. Vapormatt's patented micro nozzles deliver a controlled, targeted blast stream into restricted geometries with the precision OEM component drawings require. No other wet peening supplier has an equivalent patented solution.
Media management that doesn’t block. Sieve-based classification, standard in dry systems, blocks under production conditions. Vapormatt's patented elutriation towers remove broken and undersized media continuously without sieves, maintaining consistent slurry concentration across long production runs.
No ATEX requirement for titanium and reactive alloys. Titanium and nickel superalloys generate airborne particulate requiring ATEX-rated extraction and certified hazardous zone classification. Wet peening eliminates dust within the slurry, removing the requirement and its associated capital and compliance cost entirely.
No pre-cleaning required. Components enter the process carrying oil or grease, which is removed during peening and filtered out automatically. The separate pre-cleaning step mandated by dry shot peening specifications is eliminated altogether.
Superior surface finish at equivalent intensity. The flow of media in the water slurry produces a smoother, more consistent finish than dry peening, achieving Almen intensities up to 0.39 mm N and 0.38 mm A, often eliminating downstream polishing operations on aerofoil surfaces.
If your SPM specifies wet peening, the supplier you choose determines whether your process is audit-ready, traceable, and cost-efficient at production volume. With AMS 2432 compliant machines in use to Rolls-Royce, GE and Pratt & Whitney specifications, patented nozzle and media management technology, and over four decades of process knowledge applied to jet engine components, Vapormatt is the supplier with the longest and most thoroughly documented track record in wet peening for jet engine components.
Wet shot peening fires spherical ceramic or stainless-steel shot, carried in a water slurry, at a component’s surface to induce compressive residual stress. That stress resists fatigue crack initiation, extending the life of highly loaded rotating parts such as fan, compressor and turbine blades, blisks and discs. The water cushions each impact and carries debris away, giving a smoother finish than dry peening at the same Almen intensity.
Both methods reach the same Almen intensity, but wet shot peening carries the media in a water slurry. This gives a smoother surface finish, often removing the need to polish aerofoils. The water suppresses dust, so titanium and nickel alloys need no ATEX-rated extraction, and oil or grease is removed during peening, so no separate pre-clean is needed. Dry peening remains common where an existing specification calls for it.
Yes. AMS 2432 covers computer-monitored shot peening, and Vapormatt’s automatic wet peening machines comply with it. Shot flow, air pressure, nozzle position and cycle time are monitored in real time and logged for audit, with automatic shutdown on any deviation. For Rolls-Royce RPS428, which limits bead-to-water ratio to a maximum of 45% by volume, inline concentration measurement holds the slurry within declared limits throughout the cycle. Vapormatt machines are in use processing components to Rolls-Royce, GE and Pratt & Whitney specifications.
Laser shock peening (LSP) induces compressive residual stresses to greater depths than wet shot peening. That makes it the preferred choice where subsurface fatigue crack initiation is the primary concern, such as foreign object damage repair zones on fan blades. However, wet shot peening offers significantly lower capital and operating costs, shorter cycle times, and broader OEM approval across MRO and new manufacture workflows. For the majority of rotating engine component applications processed to Rolls-Royce, GE, and Pratt and Whitney specifications, wet shot peening delivers sufficient compressive stress depth at a production-viable cost.
AMS 2432 requires intensity to be established via a saturation curve using Almen strips of the appropriate type (N, A, or C), selected according to the target intensity range for the component. For nickel superalloy turbine discs, N-type strips are typically used where intensities fall in the lower range, while A-type strips cover the mid-range intensities common in disc fir-tree slot and bore region peening. The saturation curve must show that doubling the exposure time produces no more than a 10% increase in arc height, confirming saturation has been reached. Strip placement, holder design, and accessibility within complex disc geometry are critical variables that must be validated during process qualification.
Before a new component geometry enters serial production, a full process qualification is required under the governing specification. This typically includes saturation curve generation, coverage verification, surface roughness measurement, and residual stress confirmation by X-ray diffraction (XRD) or a similar technique. First-article inspection (FAI) documentation must show that all monitored parameters, including slurry concentration, air pressure, nozzle standoff, and cycle time, were held within specification throughout the qualification run. For AMS 2432 compliant systems, the computer monitoring records form part of the auditable FAI package. OEM-specific requirements from Rolls-Royce, GE, or Pratt and Whitney may add witness testing, laboratory analysis, or approved supplier list (ASL) registration before production release.
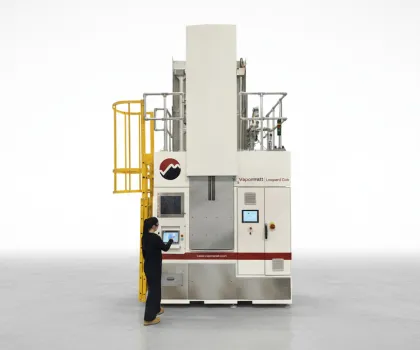
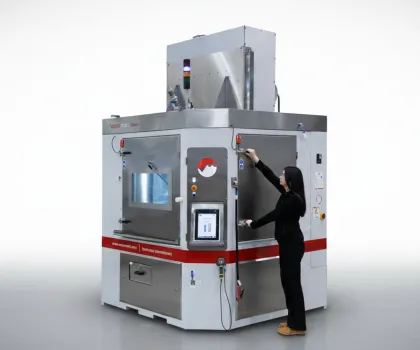
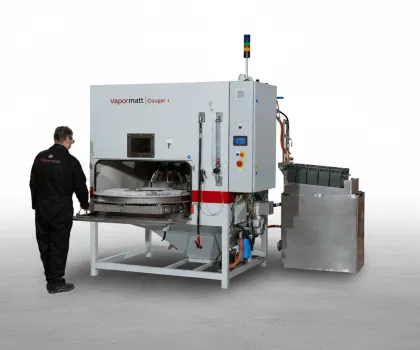
It depends on component size, geometry and throughput. The Leopard Cub is AMS 2432 compliant and suits MRO teams whose parts don’t need the full Leopard envelope. The Leopard handles large-format work such as fan blades and engine casings, with up to 8 axes and 5-tonne loads. The Sabre is a five-axis CNC cell for complex geometries. The Cougar+ offers 32 configurable options, and its vertical format suits taller parts such as fan blades.
Yes. Where appropriate, our applications engineers can run sample trials on your components at our UK R&D facility and report the results against your specification. Send us the component, its governing specification and target Almen intensity, and we’ll recommend a process and machine.