Image
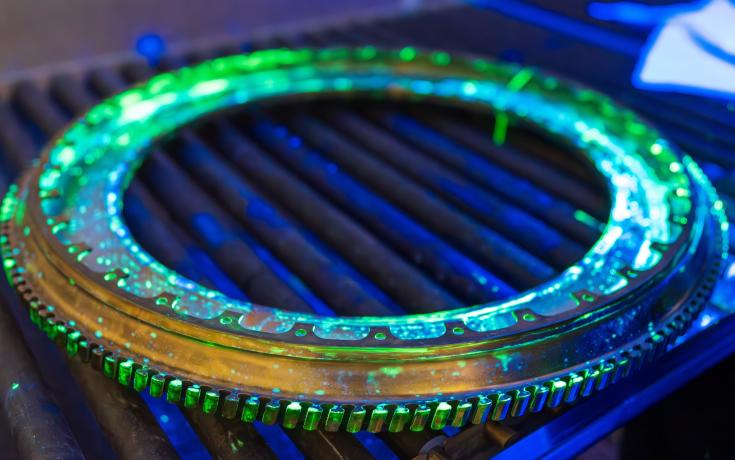
Jet engine NDT preparation is the cleaning of engine components, removing combustion deposits, heat scale, oil and carbon, so that fluorescent penetrant (FPI) and eddy current inspection see the true surface. Wet blasting does this in one controlled process, without peening over cracks or a separate degreasing stage. A surface that looks clean is not the same as a surface ready for inspection. Jet engine components arrive at your cleaning line carrying deposits accumulated across thousands of flight cycles. If any of it remains in a fir tree slot, disc bore, or blade root, you risk missed indications, false calls, and the re-inspection cost and schedule pressure that follows. The margin for error, when the component goes back on a flight-critical engine, is zero.
Replaces degreasing, blasting and drying with one operation, putting components on the inspection line faster
No peening risk, no dust, no ATEX requirement, no harmful chemicals
Every cycle produces the same result, with full parameter traceability
Approved in the specifications of Rolls-Royce, Pratt and Whitney, GE, and Airbus
Wet blasting has prepared jet engine components for NDT since the late 1940s, when Norman Ashworth, whose son Stewart later founded Vapormatt, developed the first wet blasting process while working alongside Sir Frank Whittle on the jet engine. That origin matters here: the process was created specifically to meet the surface quality demands of engine components.
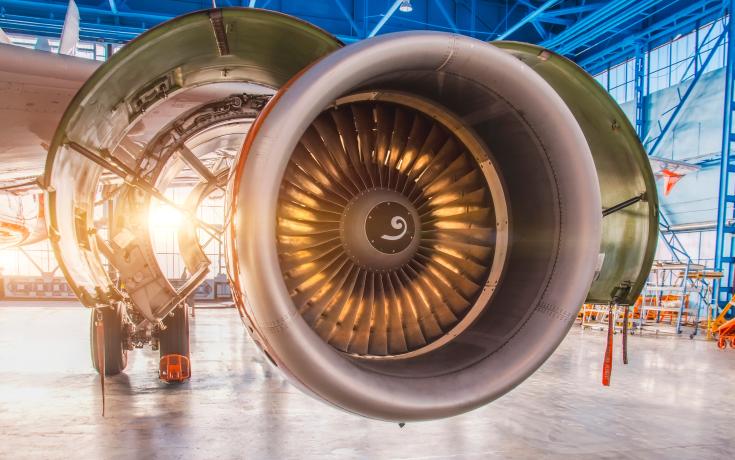
The three processes most commonly used ahead of wet blasting share a common failure: none of them reliably produce the consistent, contamination-free surface that accurate NDT depends on.
vs. dry blasting: Dry media blasting creates a fundamental conflict with NDT. The impact-driven process can peen the surface, closing the very discontinuities - cracks, micro-porosity, fatigue initiations - that the inspection is designed to find. Dry blasting also embeds media particles into the surface, adding a new source of false signal. It generates dust throughout, requiring full component cleaning and drying before inspection can proceed, adding a handling stage and time. When working with titanium engine components, dry blasting introduces ATEX filtration requirements that raise both the capital cost and the operational complexity of the process.
vs. chemical cleaning: Chemical processes can remove combustion deposits and heat scale effectively but carry their own cost. Multi-stage immersion processes - alkaline degreasing, acid etch, rinse, neutralise, dry - are time-consuming, require controlled disposal of effluent, and are poorly suited to in-line production environments. They can also attack substrate material at concentrations necessary to fully remove tenacious deposits, and they provide no mechanical action to open crack faces for penetrant entry.
vs. manual cleaning and hand scrubbing: Cleaning a typical compressor hub by hand can take several hours per part. That is a skilled inspector’s time consumed before a single measurement is taken. The result varies with operator, with fatigue, and with tool access. Complex geometries - fir tree slots, blade roots, cooling holes - are rarely fully cleaned. Residual contamination in these areas suppresses FPI penetrant migration and distorts eddy current signals, producing unreliable indications..
Find out how wet blasting compares with other finishing processes
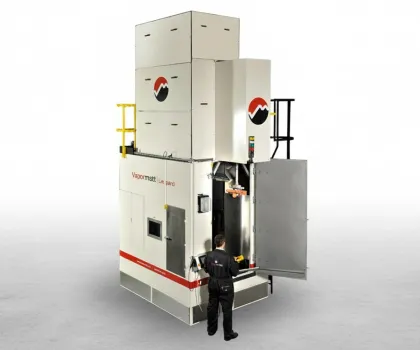
Compressor hub processing time cut from 3 hours to just 20 minutes by replacing manual wet blasting with an automatic Vapormatt Leopard Cub, which precisely blasts every angle of a hub’s complex “fir tree” geometry.
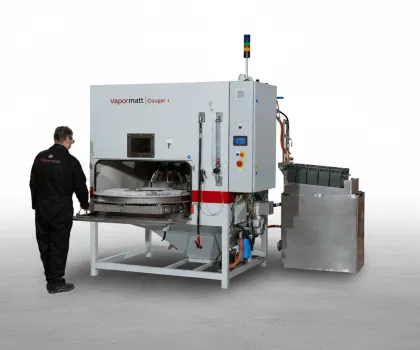
Vapormatt’s Leopard horizontal automatic wet blasting machine cut total processing time for NDT preparation from 430 hours to 88 hours (an 80% reduction) while eliminating the material loss risk associated with dry blasting.
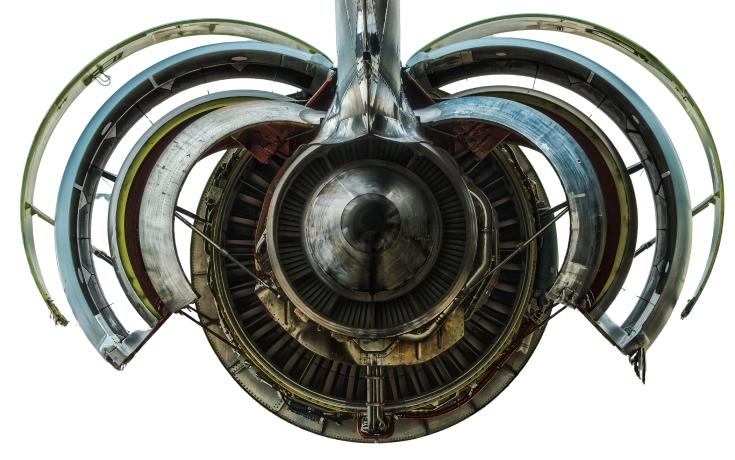
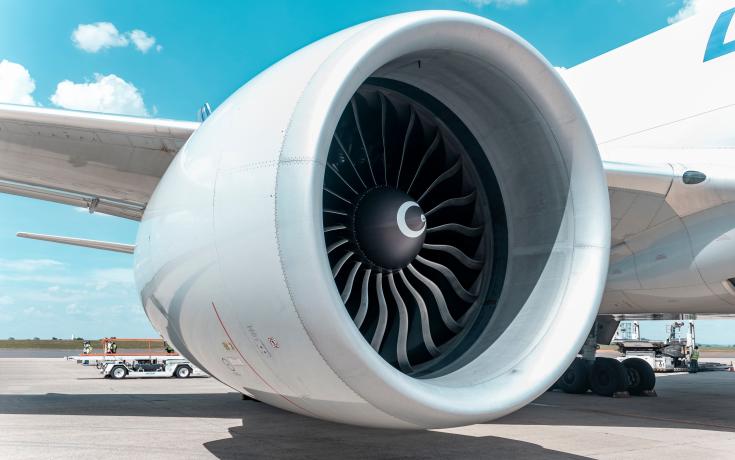
The mechanism that makes wet blasting reliable for NDT preparation is the flow of the slurry. Where dry blasting impacts, wet blasting flows. The water-carried media moves over and through complex geometries, flushing contaminants clear of blisks, discs, casing and other engine components rather than compacting them. Crack faces are opened and cleaned, not closed. The surface emerges contamination-free and ready for penetrant application without a separate degreasing stage.
couple of outcomes distinguish this from alternatives. First, no risk of peening: the wet blast recipe for NDT preparation uses flow rates and media selections specifically calibrated to prevent it, so the surface condition the inspector sees is the surface condition the component actually has. Where you do need compressive stress, see jet engine peening. This precision extends to micro nozzles, which access recessed features, cooling holes and tight geometries that conventional blast nozzles simply cannot reach, allowing wet blasting to clean deeper into a component’s architecture where competing processes fall short. Abrasive flow through these micro nozzles is equally controlled, ensuring consistent media delivery without localised pressure spikes that could compromise surface integrity. Second, process consistency: every parameter - blast pressure, slurry concentration, media grade, nozzle angle and travel speed - is monitored and recorded, producing the same result on part one and part one thousand. Robotic delivery reinforces this further, with programmed toolpaths executing repeatable, multi-axis movement around complex aerofoil profiles and internal passages, removing the variability inherent in manual handling and ensuring that each component receives exactly the same preparation regardless of operator or shift.
In one OEM’s switch from manual wet blasting to an automatic Leopard Cub, compressor hub processing fell from 3 hours to 20 minutes, with no operator intervention and every parameter recorded by Vapormatt 4.0.
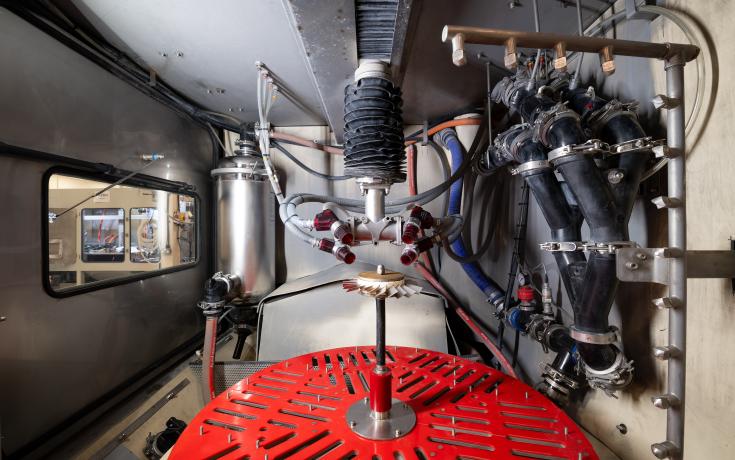
The specification record here is not incidental. Wet blasting for jet engine surface preparation is written into the approved process documentation of the OEMs whose engines your MRO facility works on. Pratt and Whitney’s SPOP16 covers wet glass bead blast cleaning. POP315-AC covers wet abrasive blasting and POP317-N covers glass bead wet blasting specifically. Rolls-Royce RPS386 and RRP56001 both cover abrasive blasting. Airbus’s AIPS02-02-003 specifies wet blasting directly by name.
These approvals exist because the process, properly controlled, delivers surfaces the inspection methods can trust. Vapormatt machines are deployed across jet engine MRO and OEM operations globally, processing compressor hubs, turbine discs, and fan blades for NDT using blast recipes developed and refined over decades of application engineering. Our case study on jet engine compressor hub NDT preparation documents the before-and-after in detail, including how automated nozzle positioning and slurry concentration monitoring produce the consistency that manual cleaning cannot.
Incomplete pre-cleaning before NDT produces one of three outcomes: a missed defect that reaches the engine, a false indication that drives unnecessary component rejection, or a re-inspection that absorbs time and cost the shop cannot afford. Wet blasting eliminates all three risks by delivering a controlled, consistent, contamination-free surface every cycle. No peening risk. No separate degreasing stage. The process was created for jet engine components. It remains the most reliable preparation method available for them.
The cost of continuing with a slower, less controlled process is measured in inspector hours, re-inspection cycles, and, ultimately, the margin for error that no engine MRO facility has.
No. Wet blasting for NDT preparation uses flow rates and media calibrated to avoid peening. The water-carried slurry flows over the surface rather than hammering it, so crack faces are opened and cleaned instead of closed. Surface-breaking defects stay visible to penetrant and eddy current inspection rather than being masked.
It depends on the specification you work to. ASTM E1417 and AMS 2647 require a pre-penetrant etch after mechanical processes that can smear metal over surface defects, unless the cognisant engineering authority approves otherwise. Our application engineers can process sample components and provide documented results to support your own approval.
Wet blasting prepares compressor hubs and discs, turbine discs, blisks, fan blades and engine casings for NDT, including titanium components. It removes combustion deposits, heat scale, oil and carbon build-up from fir tree slots, blade roots, disc bores and cooling holes. These are the areas where residual contamination most often causes missed indications.
For NDT preparation, yes. Dry blasting can peen the surface, closing the cracks the inspection is meant to find, and it leaves embedded media and dust that must be cleaned off. Chemical cleaning needs multi-stage immersion and effluent disposal, and it can attack the substrate. Wet blasting cleans in one controlled process with no peening, no dust and no harmful chemicals.
Yes. The flowing slurry reaches into fir tree slots, blade roots, disc bores and cooling passages that manual cleaning tools and dry blast media cannot consistently access. Contamination in these attachment geometries is a primary source of missed FPI indications on compressor and turbine discs. Vapormatt’s patented micro-nozzles, shown in the Leopard Cub video on this page, are a major step forward in preparing fir tree slots for NDT.
Wet blasting prepares components for fluorescent penetrant inspection (FPI), eddy current testing (ECT), magnetic particle inspection (MPI) and ultrasonic testing (UT). It supports the surface preparation requirements of ASTM E1417, AMS 2647 and ISO 3452-1, as well as OEM process approvals from Pratt and Whitney, Rolls-Royce and GE.
At one jet engine OEM, an automatic Vapormatt Leopard Cub cut stage one compressor hub preparation from 3 hours with manual wet blasting to 20 minutes. A patented micro blast gun cleans every angle of the fir tree slots. Cycle times for other components depend on their size, geometry and level of contamination.
Yes. Vapormatt 4.0 is fitted as standard to new Vapormatt machines and is available as a retrofit. It records blast pressure, slurry and abrasive concentration, and the speed of moving parts for every cycle, and the data can be accessed remotely. Within your quality management system, this record can form part of the evidence for Nadcap accreditation and OEM process approval.
Yes. Tell us the component, material, contamination and the OEM specification you work to. Our application engineers will process sample components at our UK test facility and return documented results, so you can assess the surface before committing to a wet blasting machine.