Image

If your dies aren't clean enough to inspect accurately, they aren't clean enough.
Discuss your die cleaning requirements with an applications engineer
Faster die turnaround keeps lines running with fewer stoppages
Automated wet blasting delivers the same clean-to-inspect finish every time
Gentle, controlled cleaning extends die life and reduces damage risk
Lower labour, less scrap, and higher throughput deliver rapid ROI
Every die pulled prematurely costs production time you cannot recover. Every hour your die correctors spend working on an inadequately cleaned bearing face is an hour not spent on actual correction. And every inspection that misses a fault because the die surface was not clean enough sends that problem to the press.
Die shop efficiency lives or dies on the quality of your cleaning process. If your current method leaves residual aluminium, discolouration, or caustic trace on the bearing surfaces, everything downstream, inspection accuracy, correction quality, and die success rate, is compromised before it begins.
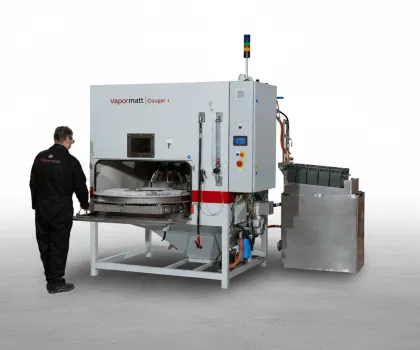
Wet blasting cleans aluminium extrusion dies after the caustic soda dip. A slurry of fine abrasive and water removes residual aluminium, carbonisation, discolouration and caustic trace from bearing surfaces and porthole ports, without changing bearing geometry. The Vapormatt Cougar+ handles dies from 70mm to over 1,100mm in diameter and up to 300 dies a day, leaving them ready for inspection, correction or nitriding.
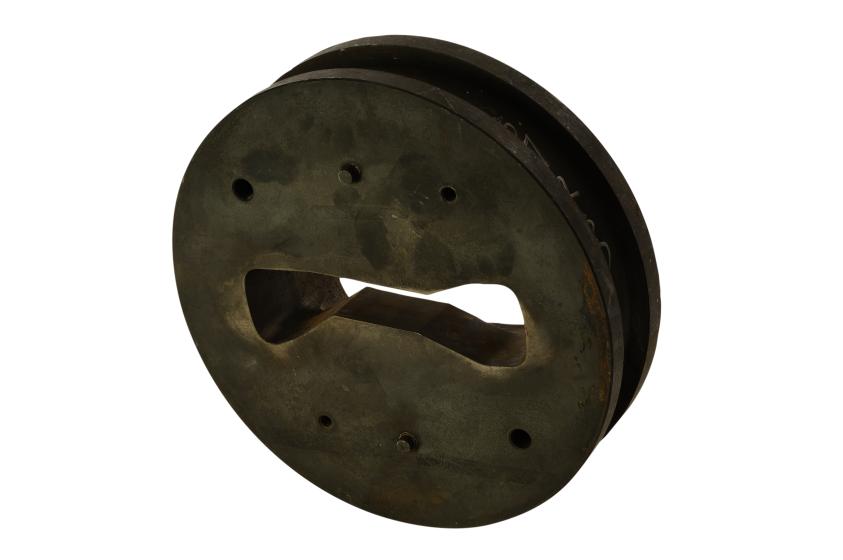
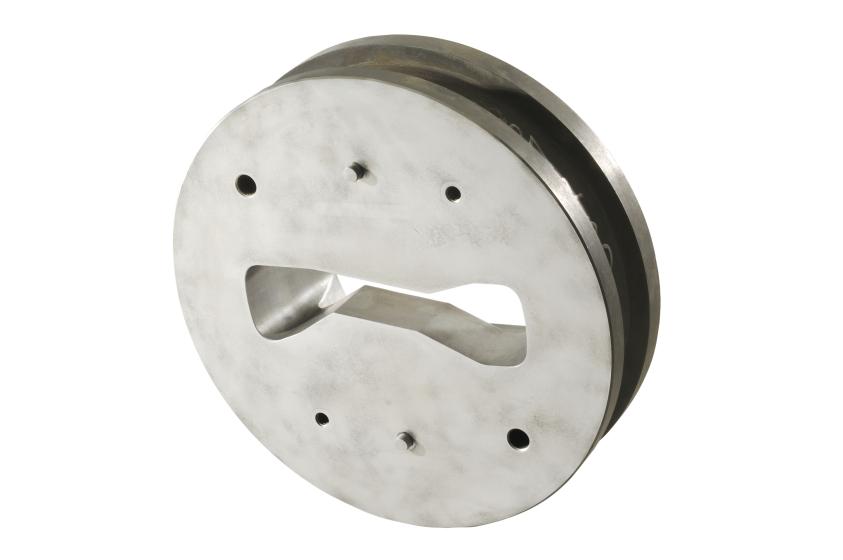
The caustic soda dip is essential, but it is not sufficient. It removes bulk aluminium effectively. What it leaves behind, fine residual particles, carbonisation, discolouration from heat and pressure, is precisely what makes accurate die inspection difficult.
vs. shot blasting: Steel shot removes contamination aggressively but with poor control over the bearing surface. Complex port holes and intricate bearing profiles are not reliably reached, and the process cannot begin until the die is fully dried after the caustic rinse, adding non-productive time to every cleaning cycle. The abrasive impact also risks unwanted material removal at the die edges: the sharp, precise geometry that defines the bearing surface can be dulled or deformed, requiring corrective work before the die returns to press.
vs. manual polishing: Skilled die correctors are expensive and finite. Applying their time to cleaning work that a machine should handle is a structural inefficiency that compounds across a full day's die volume.
Find out more about wet blasting vs. other finishing processes
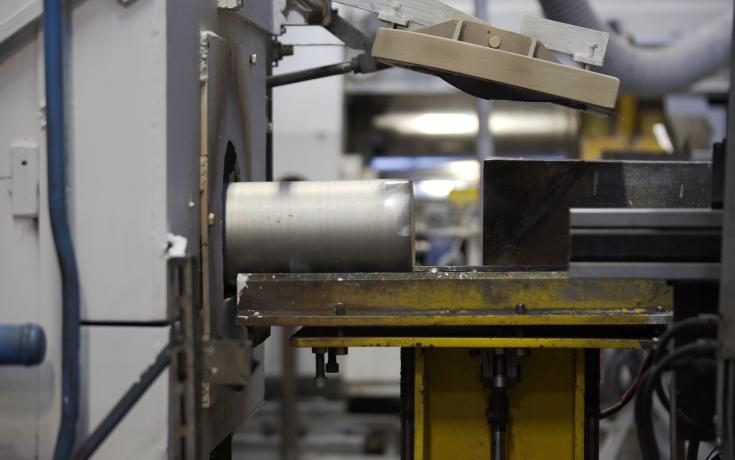
Wet blasting works differently at a mechanical level. The slurry, a calibrated mixture of abrasive media suspended in water, is propelled under controlled pressure through nozzles positioned above the die. The water lubricates the abrasive particles as they flow across the bearing surface, allowing the slurry to navigate complex port geometries uniformly, cleaning where shot cannot reach, without altering die profile geometry.
Three outcomes result directly from this mechanism:
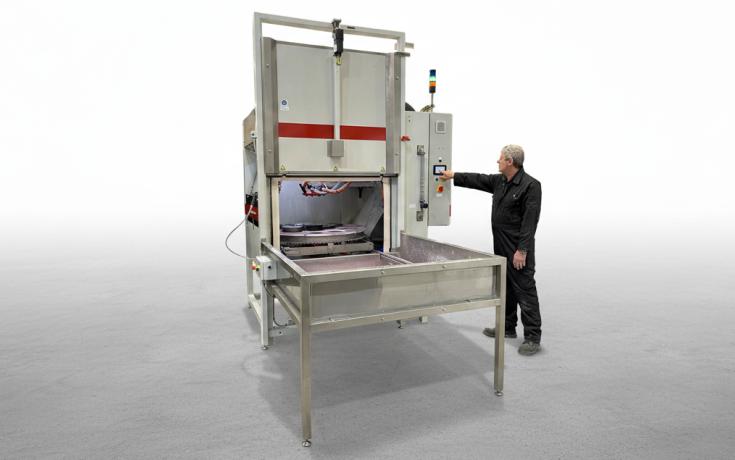
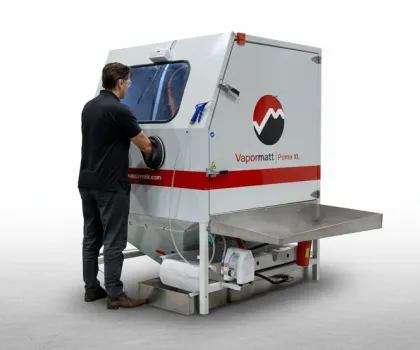
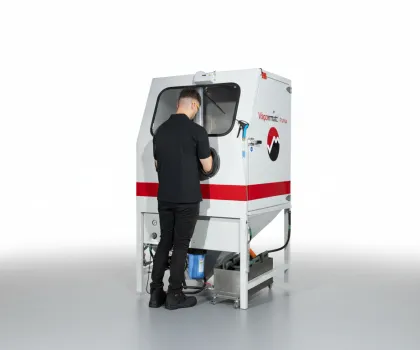
Vapormatt machines handle dies from 70mm (2.5") to over 1,100mm (43") in diameter, and from around 8kg for small architectural profile dies to 250-300kg for large structural tooling. For the largest dies, running into several tonnes, Vapormatt builds heavy duty machines to specification.
Throughput scales to your operation. Smaller die shops processing 5 to 10 pieces per day use the single load-end Cougar+ configuration. High-volume operations processing up to 300 pieces per day run the double load-end configuration, where one turntable loads while the other cleans, removing dead time from the cycle entirely.
A US window and door extruder now cleans around 240 dies a day on a Vapormatt Cougar, with fewer pulled dies, higher extrusion recoveries and longer die life.
Read the US extruder case study
Learn more about the Cougar+ in single load end configuration
“The machine works well and does a great job at cleaning dies.”
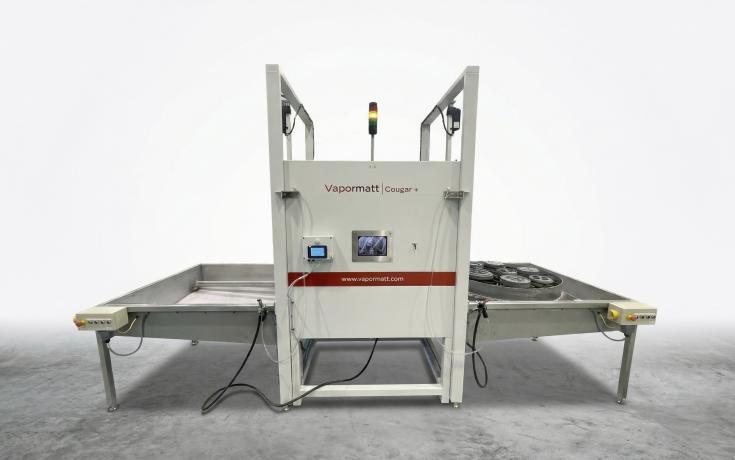
Extrusion die shops are demanding environments. Dies arrive hot, heavy, and contaminated. They are moved by overhead crane at production speed. Caustic residue, aluminium fines, and process water are constant. The Cougar+ is built for this, with turntables rated to 1,000kg (2,200lbs), enclosures engineered to resist continuous caustic and abrasive exposure, and wear components selected for die shop reality, not laboratory conditions.
Machine downtime in a die shop is a direct constraint on press output. Vapormatt has been manufacturing wet blasting machines since 1978 with more than 2,000 machines installed in over 50 countries. The company is family-owned, and remains solely focused on wet blasting.
Learn more about the Cougar+ in double load end configuration
A die shop running shot blasting or manual polishing carries costs it does not need: extended cleaning cycles, inconsistent bearing surface quality, and die corrector time spent on preparation rather than correction. Wet blasting eliminates each of these at the source. Dies leave the machine clean enough for accurate inspection, geometrically intact, and ready for correction or nitriding.
The most useful next step is a direct conversation. Tell us your die volumes, your profile mix, and where your current process is costing you -- we will tell you exactly what the improvement looks like.
For most die shops, the most effective method is a caustic soda dip to remove bulk aluminium, followed by wet blasting. Wet blasting removes the residual aluminium, carbonisation, discolouration and caustic trace that the dip leaves on bearing surfaces and in porthole ports, without changing die geometry. Dies come out clean enough to inspect accurately and ready for correction or nitriding.
No. The caustic dip removes bulk aluminium, and wet blasting follows it to remove the fine residue the dip leaves behind. Unlike shot blasting, it doesn’t need the dies dried after the caustic rinse, so they go straight from rinse to wet blasting with no waiting time. Tell us about your current process and we’ll show you what changes.
Shot blasting cleans aggressively but gives little control at the bearing surface. It can dull or deform die edges, does not reliably reach complex port holes, and needs dies to be fully dried first. Wet blasting cushions the abrasive in water, so it cleans porthole and multi-void dies uniformly, leaves bearing edges intact and removes caustic trace in the same cycle.
No. Water cushions the abrasive particles throughout the process, which prevents the edge damage associated with shot blasting. Bearing surface geometry and die profiles stay intact, and the fine, uniform finish makes inspection and correction more accurate, not less.
Yes. The water lubricates the abrasive, so the slurry flows into complex geometries that shot blasting cannot reliably reach, including the internal port surfaces of porthole dies and multi-void profiles. This is one of the main reasons die shops with a complex profile mix move from shot blasting to wet blasting.
Yes. Wet blasting cleans and finishes bearing surfaces in one automated cycle, giving the same result on every die whoever is on shift. Die correctors spend their time on correction rather than cleaning. New Zealand extruder Altus uses its Vapormatt Cougar to polish critical bearing surfaces without altering die profiles.
Yes. Wet blasting leaves the die surface in an activated state that aids nitrogen diffusion during nitriding, and extruders report better nitride adhesion. A corrosion inhibitor can be added to the system to stop dies oxidising before nitriding or in storage. Dies that are not nitrided benefit equally: the process is specified for cleaning quality, not just coating preparation.
Vapormatt machines clean dies from 70mm (2.5") to over 1,100mm (43") in diameter, weighing from around 8kg to 250–300kg, on turntables rated to 1,000kg (2,205lb). The single load-end Cougar+ suits die shops cleaning 5 to 10 dies a day, and the double load-end Cougar+ handles up to 300 a day. Heavy-duty machines for multi-tonne dies are built to specification.
Yes. Wet blasting produces no airborne dust, which is the main health risk of dry shot blasting. The process runs inside a sealed enclosure, effluent is filtered and recirculated, and solid waste is separated for disposal. Vapormatt machines typically run at around 75 dB(A), below the 80 dB(A) level at which UK hearing protection duties begin.