Image
Wet blasting prepares metal and composite surfaces for adhesive bonding in a single step. It removes the resinous or oxidised layer and leaves a controlled Ra profile and a high-energy surface the adhesive can wet out on. A bond that looked right on the line can still fail in service if that preparation is inconsistent.
Wet blasting removes the resinous or oxidised surface layer cleanly and consistently, as well as creating a highly reactive surface and profile to which adhesives and coatings can grip. The controlled slurry cushions the abrasive at the point of impact, which means the surface is keyed without being torn - especially important when bonding composites as incorrect surface preparation will damage fibres and consequently weaken the structure. The result is repeatable across an entire batch, not dependent on operator pressure or dry conditions.
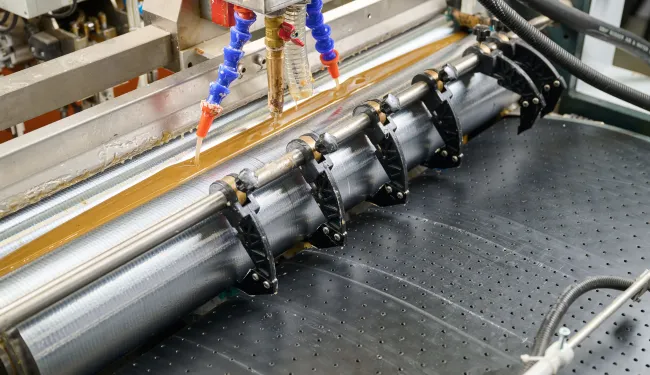
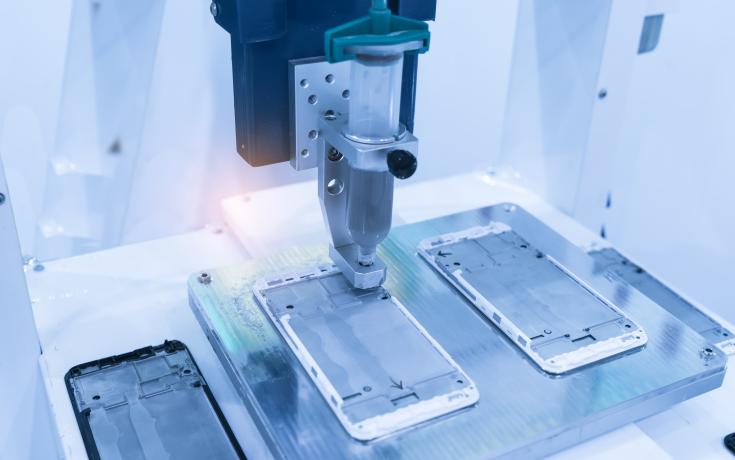
The slurry carries abrasive particles to the surface in a column of water, which simultaneously cleans and profiles in a single cycle. Water dampens the impact energy, preventing the micro-fractures and embedded contamination that undermine bond strength. Pressure, abrasive grade, and gun angle can each be adjusted independently, giving you precise control over the surface profile you achieve.
Typical setup: surface finishing for bonding preparation
The parameters below are indicative and confirmed for the component types listed. Results for other geometries and materials may vary.
| Component type | Typical size or weight | Process mode | Achievable outcome | Minimum control |
|---|---|---|---|---|
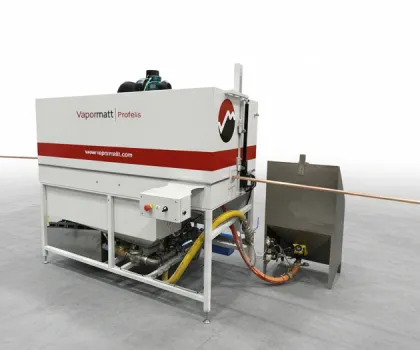
| Aluminium rod (wire) | Ø10 mm | Automatic | 3.5 to 7 µm Ra; good bond strength | Continuous automatic machine (Profelis) |
| Bonded studs and standoffs | Ø8 to 50 mm x 5 to 50 mm tall | Automatic | 3.2 to 6.3 µm Ra | Automatic machine |
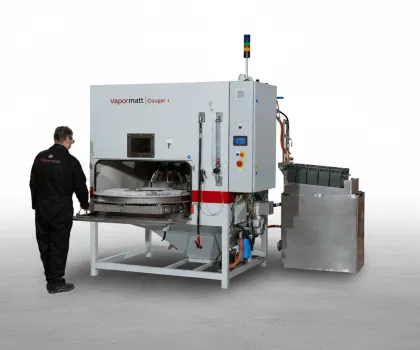
| Composite panels | 300 x 300 mm | Manual | Resinous surface layer fully removed; homogenous finish passing water break test | Basic manual machine |
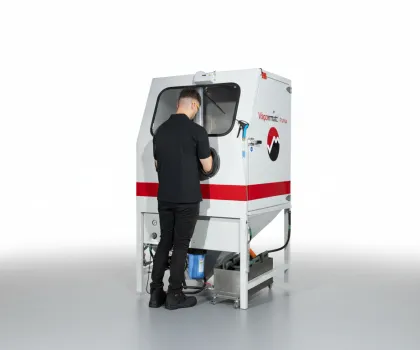
In Vapormatt sample processing trials, composite panels for G1c fracture testing were processed on a Cougar wet blasting machine using APA180/220 blast media at 2.5 to 4.0 bar. All panels achieved a homogenous finish that passed water break tests, with the resinous layer fully removed and samples confirmed ready for structural bond strength testing.
Bonding preparation requirements also arise across aerospace structural assemblies and composite structures, where surface consistency is directly linked to joint integrity. For applications in those sectors, see how wet blasting is used in aerospace MRO operations and across carbon fibre composite bonding preparation.
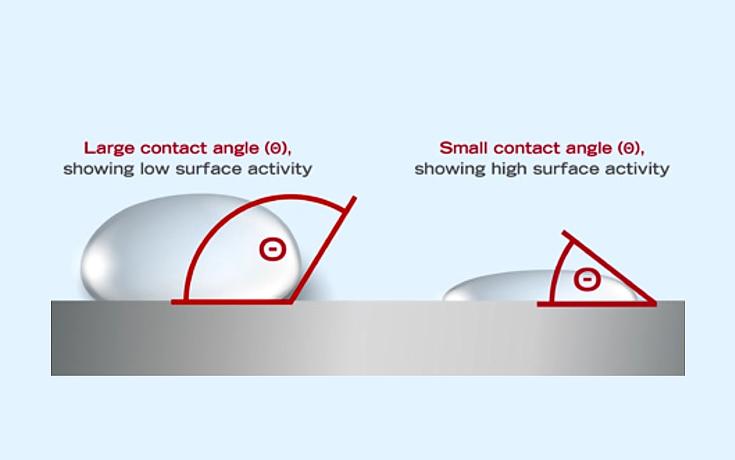
Wet blasting leaves a hydrophilic, high-energy surface, so adhesive spreads across the joint instead of beading. This is measured as the water contact angle: the lower the angle, the better the wet-out. In Vapormatt testing on carbon fibre, wet-blasted surfaces measured 43-48°, against 86° for dry grit blasting and 88° for manual sanding. They stayed at 43-54° for 17 days after blasting. A goniometer gives the precise measurement; a water break test gives a quick pass/fail check on the shop floor.
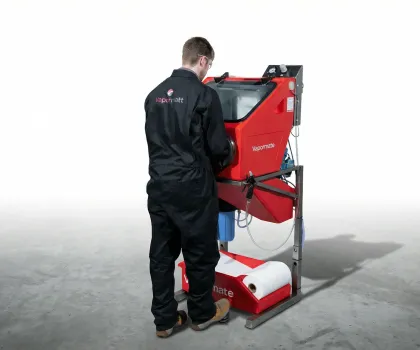
"Our Vapormate has without doubt stood the test of time and saves us a lot of man hours. It is also very consistent and reliable."
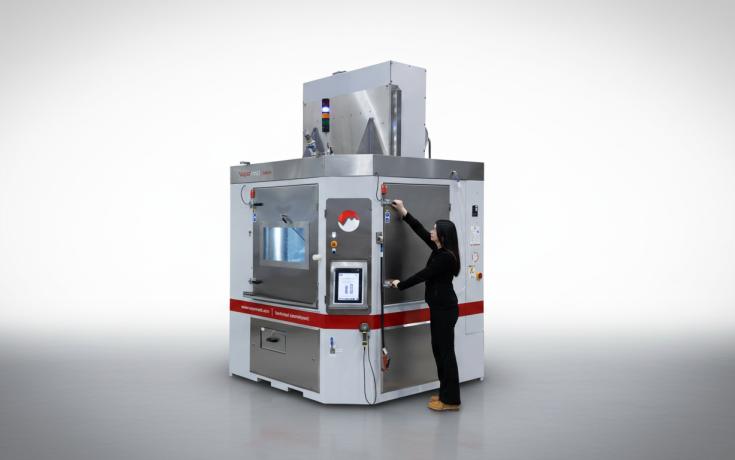
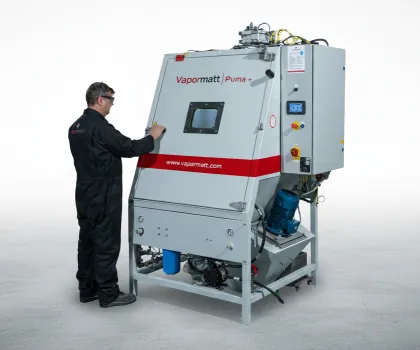
Vapormatt's wet blasting machine, installed at the National Composites Centre in Bristol, is transforming composite bonding performance by delivering clean, precision-abraded surfaces on materials like carbon fibre and GRP - without causing fibre damage.
Wet blasting gives a cleaner, more wettable and more repeatable surface than dry grit blasting or manual sanding. The water cushions the abrasive, so the surface is profiled without the micro-fractures, embedded contamination and dust that dry blasting can leave. Unlike sanding, the result doesn’t depend on the operator. In Vapormatt testing on carbon fibre, wet-blasted surfaces measured a water contact angle of 43-48°, against 86° for dry grit blasting and 88° for manual sanding.
For aluminium and steel fastener-type components, sample processing trials show Ra values of 3.2 to 7 µm, depending on the abrasive grade and pressure applied.
Not at correctly set pressures. In Vapormatt sample processing trials on composite panels, the working range was 2.5 to 4.0 bar (36 to 58 psi) using APA180/220 media. Fibre damage was seen only above 4.5 bar (65 psi), which is outside the recommended range for composite substrates. For more detail, see carbon fibre composite bonding preparation.
Use a water break test. A correctly prepared surface holds a continuous water film without beading. The test takes under a minute and needs no specialist equipment. For a measured result, use a goniometer to check the water contact angle. Wet-blasted carbon fibre typically measures 43–48° in Vapormatt testing.
In Vapormatt testing on carbon fibre, the water contact angle stayed between 43° and 54° for 17 days after blasting, so parts don’t have to be bonded immediately. Run a water break test before bonding to confirm the surface is still ready for your adhesive.
In automatic processes, gun positioning is set to give full coverage, and pressure is held within the specified range throughout the run. Batch-to-batch variation is controlled by the machine parameters, not the operator. For critical applications, process logging records the parameters used for each batch as evidence of consistency.
Yes. Metals and composites need different parameter sets, but the same machine can run both with a recipe change between batches. Typical starting points are 46 to 120 mesh aluminium oxide at 3 to 5 bar (44 to 73 psi) for metals, and APA180/220 at 2.5 to 4.0 bar (36 to 58 psi) for composites.
Yes. Where appropriate, Vapormatt applications engineers run sample trials on your own components at our R&D facility, so you can see the bonding preparation result on your own parts before choosing a machine.