
The production challenge
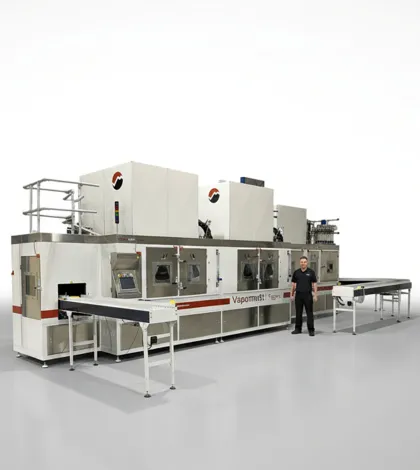
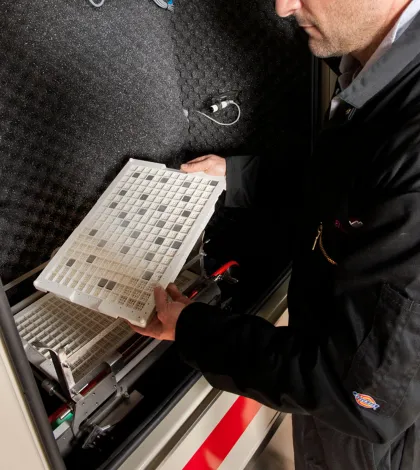
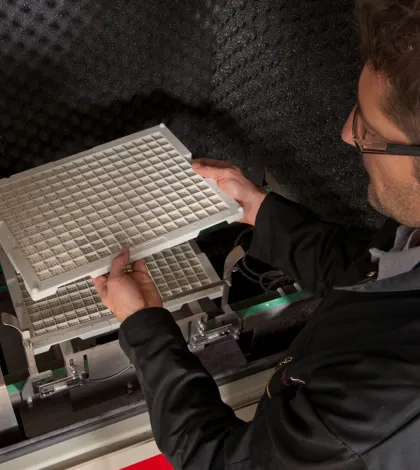
In high-volume insert production, throughput and consistency are in direct tension. Running faster risks tolerance drift, and every non-conforming pallet carries a scrap cost that compounds fast. The Tiger+ resolves that tension with two fully independent blast chambers in one in-line system: one conveyor, one recipe architecture and one acceptance process.
Process control and compliance
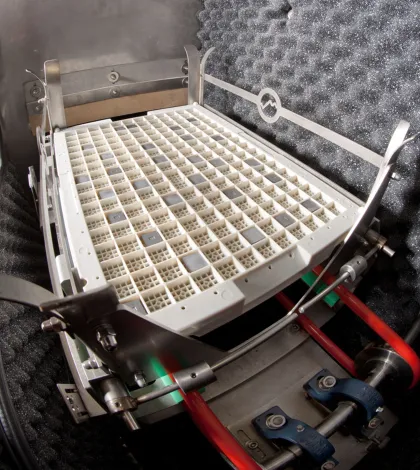
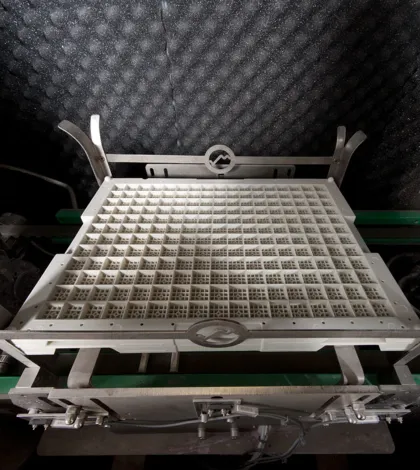
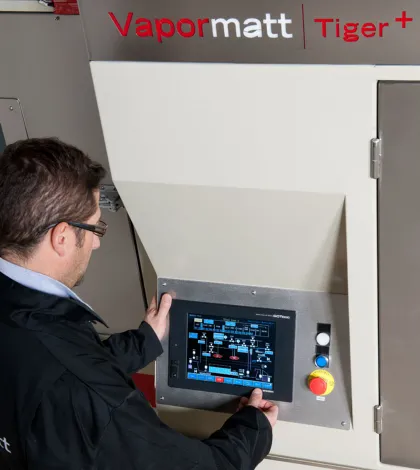
Each blast zone runs under its own recipe, with up to 999 recipes stored on the password-protected HMI. A CNC servo gantry in each zone positions the gun crowns to better than ±0.5mm (19.7 thou) on the Y axis, while closed-loop slurry pressure control compensates for nozzle and hose wear. With the patented elutriation tower fitted, broken-down abrasive is continuously removed from each zone’s slurry circuit, keeping media quality consistent in both chambers without manual intervention. Every parameter is logged and every cycle is reproducible to ±5µm (0.2 thou), with post-process reporting and MES integration available.
Why Vapormatt
The Ashworth family invented the wet blasting machine in the late 1940s, and Vapormatt has built nothing but wet blasting machines since 1978. We built the first automated edge honing machines for cutting tool inserts in the 1980s, hold the patent for K-factor edge control by wet blasting (GB2590936B), and have supplied more than 2,000 machines to over 50 countries.
- Dual-chamber architecture: Two separate blast chambers, each with its own slurry pumps, abrasive and recipe, run different processes in sequence or the same process in parallel. That is what separates the Tiger+ from the single-chamber Tiger: a coarser abrasive can hone the edge in chamber one while a finer abrasive polishes it in chamber two, without a second machine, qualification or maintenance programme.
- Patented elutriation tower: Specified for each blast zone on edge honing applications, it continuously removes broken-down abrasive finer than the selected grade, so media specification and edge radius stay consistent over long production runs. No equivalent exists on competing machines.
- Vapormatt 4.0 connectivity: Remote diagnostics, machine status, maintenance history and just-in-time spare parts through Vapormatt’s IIoT dashboard, with 12 months’ subscription included on every new machine. Minimises unplanned downtime on a machine running at maximum capacity.
- Specified for your inserts: Tell us about your inserts, target edge radius and production volumes, and our applications engineers will recommend the right process and machine configuration, with an indicative budget.
The Tiger+ also carries further patented process and nozzle technologies.
Vapormatt patents and process innovation
The Vapormatt Promise: every Tiger+ is tested against the agreed specification at factory and site acceptance.
The bottom line
No other in-line wet blasting machine combines two separate blast chambers, each with its own slurry circuit, with ±5µm consistency proven under factory and site acceptance testing. When carbide is a strategic material, tolerance drift is not a quality problem; it is a direct commercial loss on every pallet. If one honing process at high volume is enough, the Tiger is built for that, and the Jaguar suits batch processing without an integrated wash and dry line. If you need edge honing and polishing in one pass, or double the throughput of a single chamber, the Tiger+ is the specification. Tell us about your inserts and we will recommend the right machine for your volumes.
Technical specifications
| Parameter | Specification |
|---|---|
| Applications | Edge honing, deburring, cleaning and cobalt skin removal, pre- and post-coating polishing, selective coating removal, post-coating peening |
| Installed dimensions (L × W × H) | 10.3m × 2.05m × 3.3m (406" × 81" × 130"); minimum installation space 11.9m × 3.85m × 3.5m (469" × 152" × 138") |
| Machine weight | 8,000kg (17,650 lb) empty; approx. 9,500kg (20,950 lb) with water and abrasive |
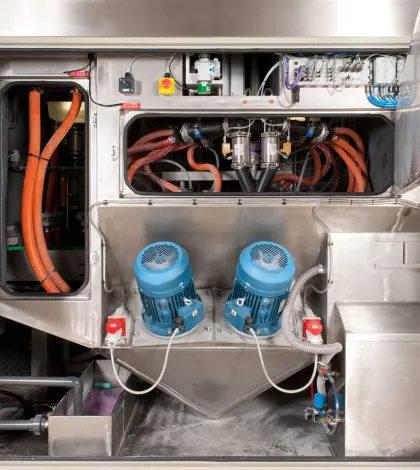
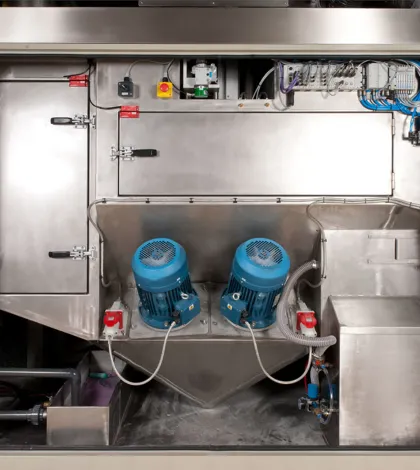
| Blast chambers | 2 independent blast zones, each with its own slurry circuit and 2 Vapormatt 5.5kW vortex pumps |
| Blast guns | 16 × Mk3 Vapormatt blast guns per zone with boron carbide nozzles, in 2 independently controlled 8-gun crowns; Mk 9 guns optional |
| Gun crown configurations | 60°, 55°, 45°, 80°, or manually adjustable 45°/80° |
| Edge hone capability | Up to 70µm (2.8 thou), held to ±10% or ±5µm (0.2 thou), whichever is larger, subject to pre-process insert condition |
| Blast media | Aluminium oxide, FEPA 60 to FEPA 320 |
| CNC gantry Y-axis stroke per zone | 700mm (27.6"); max speed 200mm/s; accuracy ±0.5mm |
| Vertical gun head manipulator (Z-axis) | 400mm (16") stroke (optional) |
| Pallet capacity (auto-load magazine) | Up to 20 pallets; 40kg (88.2 lb) max load |
| Compatible pallet sizes | Wendt 296 × 246mm (12" × 10"); Manz 383 × 281.3mm (15" × 11") |
| System throughput (gantry configuration) | Minimum 16 pallets/hour after first pallet complete (one pallet every 3 min 45 s) |
| Process stages | 11: macro wet blast 1 and 2, rinse 1 and 2, micro wet blast 3 and 4, pre-rinse, drag rinse, ultrasonic dunk (optional), final DI rinse, hot-air dry |
| Controls | Touchscreen HMI with password-protected logins, up to 999 stored recipes, post-process reporting and preventative maintenance alerts |
| Automation options | RFID readers, barcode scanners, gantry robot pallet transfer, infeed/outfeed roller conveyors, flipping unit, 30-pallet load and unload magazines, AGV-compatible cart docking, MES integration |
| Construction | Corrosion-resistant high-grade stainless steel cabinet with watertight enclosure |
| Noise level | Specifiable to 75 dBA |
| Power supply | 400/480V, 3-phase, 50/60Hz, 69kW (110A at 400V, 50Hz) |
| Process air | 6–7 bar (90–100 psi); max 22.4 Nm³/min (800 SCFM) at 4 bar |
Full technical specifications are available in the downloadable Tiger+ machine brochure