Image

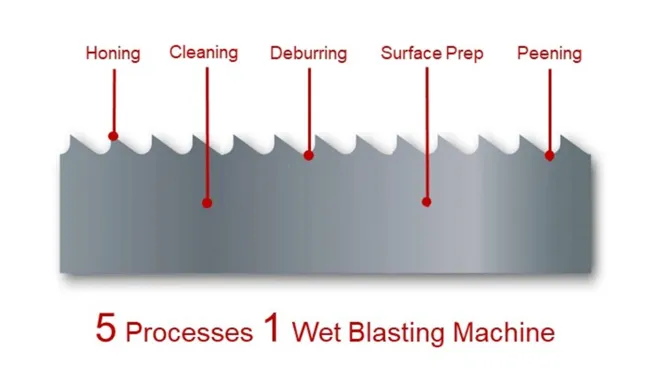
Wet blasting (also called vapor blasting) hones carbide teeth, peens gullets and cleans bandsaw blades for coating in one in-line pass, so blades cut at full speed from the first stroke with no break-in period.
Talk to an applications engineer about your blade finishing requirements
Carbide teeth are honed to an exact edge radius, eliminating chipping from first cut
Gullet peening creates -1,500 MPa compressive stresses, preventing fatigue cracks
Burrs, heat marks, and notches removed in a single pass, ready for coating
Inline processing integrates directly into your production line, maximising throughput
Your customers expect a blade that performs from the first cut. Carbide teeth that chip on contact, gullets that crack under load, and a surface that won't retain cutting lubricants are not acceptable failure modes. They are unhappy customers, returns, and lost repeat orders waiting to happen.
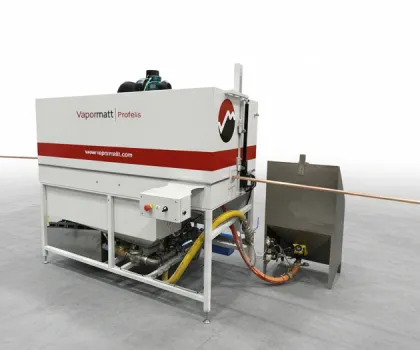
The unique Vapormatt Profelis automatic wet blasting system resolves all three (chipping, gullet cracking and poor lubricant retention) in a single in-line operation. Vapormatt has supplied bandsaw blade finishing systems globally since 1998, processing coil-to-coil blades up to 100mm and loop blades up to 370mm in height.
Learn more about the Vapormatt Profelis in-line automatic wet blasting system
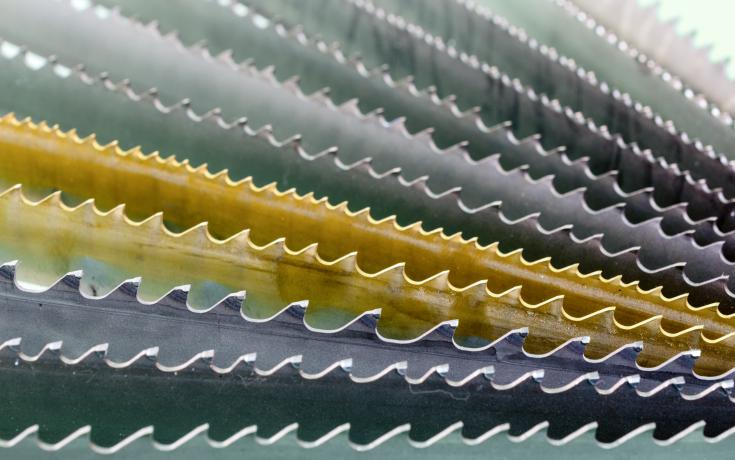
Dry blasting and dry shot peening remain common in bandsaw blade production. They clean and peen to a degree. But they cannot hone a carbide tooth accurately, they generate dust that forces the process off-line into a sealed room, and they leave a surface that is less reactive and less consistent than wet blasting achieves.
Wet blasting uses a controlled slurry of water and abrasive media. The water cushions impact, giving finer control over surface energy and finish consistency than dry processes allow. It delivers three outcomes in a single pass that dry alternatives cannot replicate together: tooth honing, gullet peening and cleaning.
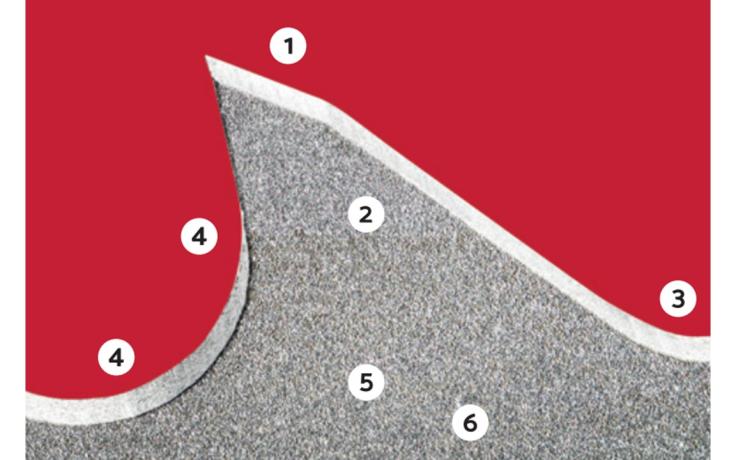
1. Carbide tooth honing
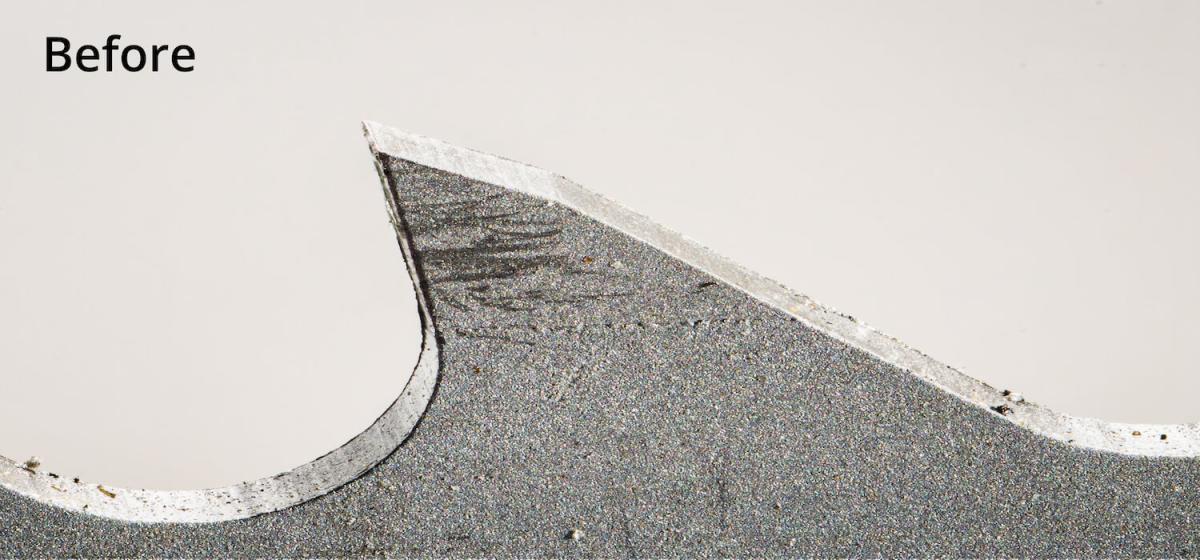
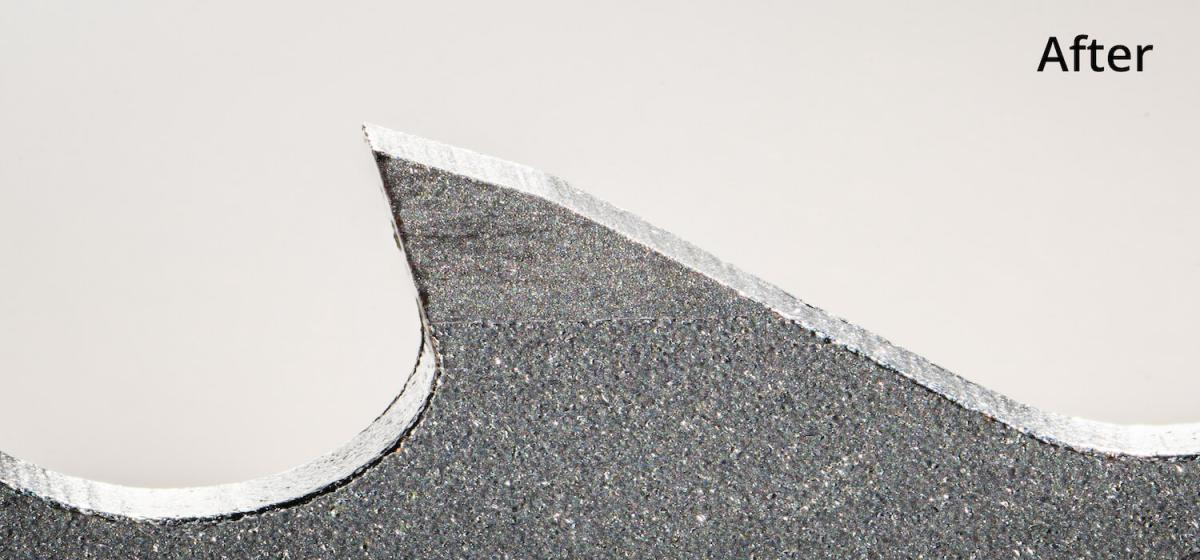
A freshly formed carbide tooth is sharp but fragile. Without a controlled edge radius, it chips under load. With wet blasting, a defined hone is applied to each tooth, reducing the risk of tooth breakage and chipping from the first cut. Edge radius increases from approximately 3µm to 20µm in a single pass. The blade cuts at full speed from installation, with no break-in period absorbing your customer’s production capacity.
2, 3, 5, 6. Surface cleaning, deburring and coating preparation
Wet blasting removes burrs, heat marks, heat scale and machining notches in a single pass. It creates a clean, cosmetic finish with a surface roughness that improves oil retention significantly compared to dry blasting. Blades arrive at downstream processing clean, dried, reactive, and ready for coating, painting, branding and anti-rust treatments.
4. Micro-nozzle gullet and teeth braze point peening
The gullet is the weakest point in any bandsaw blade under cyclic load. Punching can level tensile residual stresses in the surface layer of up to +1,000 MPa, stress that accelerates fatigue crack initiation under repeated flexing. Peening reverses that. A large European bandsaw blade manufacturer and Vapormatt customer achieved compressive residual stresses of approximately -1,500 MPa at the surface layer: a shift of 2,500 MPa from the tensile baseline left by punching. Wet peening also increases the compressive stress of bandsaw tooth braze points.
Cracks do not propagate in a surface under compression. Vapormatt's micro-nozzle configuration delivers that compressive stress state specifically to the gullet, where fatigue failure begins.
"Our old dry blasting machine was a bottleneck in the production process."
Vapormatt has been engineering wet blasting systems for bandsaw blade manufacturers since 1998, with systems running in production lines globally. Pilana Metal switched from dry blasting to an in-line Vapormatt system, increasing line speed from 1.5m per minute to 8m per minute and permanently discontinuing dry blasting as a result.
Read the Pilana Metal case study
Two things distinguish our approach:
The Vapormatt Promise: the machine meets the agreed specification, or we make it right.
A blade that cuts hard from the first stroke, without chipping, without forcing your customer through a break-in period, and with a surface that retains oil through storage, commands a premium price and earns repeat orders. Without in-line wet blasting, that finish is not consistently achievable. With it, it is engineered in.
Wet blasting is an in-line finishing process that hones carbide teeth, peens gullets and cleans bandsaw blades in a single pass. It is also called vapor blasting. A slurry of water and abrasive media is blasted onto the blade; the water cushions each impact, giving precise control without dust. Blades leave the machine rinsed, dried and ready for coating, branding or packing.
Wet blasting applies a controlled edge radius to every tooth, taking carbide teeth from around 3µm to 20µm in a single pass. Radii from 5 to 50µm are achievable to suit the blade and application. A honed tooth resists chipping from the first cut, so the blade runs at full speed from installation with no break-in period. Learn more about edge honing
Peening replaces the tensile stress left by punching with compressive stress, and cracks do not propagate in a surface under compression. Punching can leave tensile residual stresses of up to +1,000 MPa in the gullet. A Vapormatt customer achieved approximately -1,500 MPa of compressive stress after wet peening, a shift of 2,500 MPa. Wet peening also strengthens tooth braze points.
Wet blasting hones, peens and cleans in one in-line pass, which dry blasting cannot do. Dry blasting cannot hone carbide teeth accurately. It also produces dust that usually forces it off the production line into a sealed room, and it leaves a less reactive, less consistent surface. Because wet blasting is dust-free, it runs in-line with no off-line transfer.
Yes. Impact energy is set precisely through slurry concentration, nozzle angle and media grade. That makes it possible to hone carbide teeth without fracturing the edge while peening the gullet and cleaning the blade body in the same pass. Coil-to-coil and loop blades, single-sided and double-sided, can all be processed.
The media is matched to the blade and the result required:
Our abrasive and blast media guide explains how each media type behaves.
Wet blasting removes burrs, heat marks, heat scale and machining notches. It leaves a clean, reactive surface that coatings, printed branding and anti-rust treatments bond to well. The surface also holds protective oil better than a dry-blasted one, so blades resist corrosion in storage. An integrated rinse and dry means blades go straight to the next process. Learn more about coating preparation
Wet blasting runs at production line speed rather than creating a bottleneck. Pilana Metal, a Czech bandsaw blade manufacturer, increased line speed from 1.5 metres per minute with its previous dry blasting machine to 8 metres per minute with an in-line Vapormatt Profelis. It now runs the machine across three shifts a day.
The Vapormatt Profelis is the in-line wet blasting machine for bandsaw blades. It processes coil-to-coil blades up to 100mm and loop blades up to 370mm in height. A multi-gun gantry and micro-nozzle configuration target the teeth and gullets. The machine is fully enclosed, recycles its slurry in a closed loop, and fits into existing production lines. Vapormatt has supplied bandsaw blade finishing systems since 1998.
Yes. Send us sample blades and our applications engineers will process them in our R&D facility to your target edge radius and finish. They’re returned with measurements and a test report, so you can judge the result on your own blades before a machine is specified.