Image

Wet blasting (also known as vapor blasting) strips paint, corrosion and contamination from aluminium and composite propeller and helicopter rotor blades, and prepares them for NDT, recoating or bonding in one controlled pass. The water cushions the abrasive, so fibres and substrate are left undamaged and surface cracks stay open for penetrant inspection. Vapormatt has supplied rotor blade wet blasting machines since 1982.
Talk to an applications engineer about your blade finishing requirements
Water cushions the abrasive on impact, leaving fibres and substrates undamaged
Creates a fully activated surface where adhesives and coatings bond completely
The flowing slurry opens cracks rather than concealing them, improving NDT accuracy
Every parameter is controllable, delivering the same verified finish every cycle
Every blade that leaves your facility is released with an authorised release certificate (EASA Form 1 or FAA 8130-3).
OEMs need the same bond-ready finish on every composite blade, cycle after cycle. MRO shops need paint off metallic and composite blades without substrate damage, on a surface that exposes cracks rather than hiding them. Wet blasting does both in one controlled, recordable operation.
vs. Manual sanding and hand finishing: Slow and aggressive, with no process record and no repeatability guarantee. On composite blades, sanding risks fibre damage. Finish quality varies between operators and cycles, making bond strength inconsistent. Hand arm vibration risk is present throughout.
vs. Chemical stripping: Effective at removing paint but the compliance burden is significant. Multi-stage handling, solvent residue clean-up, COSHH controls and PPE all add time and complexity. For aluminium blades going to dye penetrant NDT, chemical residues in surface micro-cracks can mask defects and compromise results.
vs. Dry blasting: Cannot degrease simultaneously, so a separate cleaning stage is always required before or after. On metallic blades, dry blasting closes surface cracks rather than opening them, which is the wrong outcome for NDT preparation.
Find out how wet blasting compares with other finishing processes
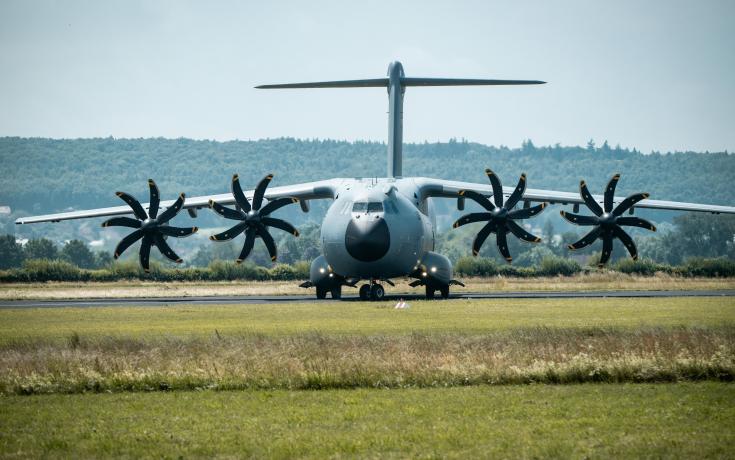
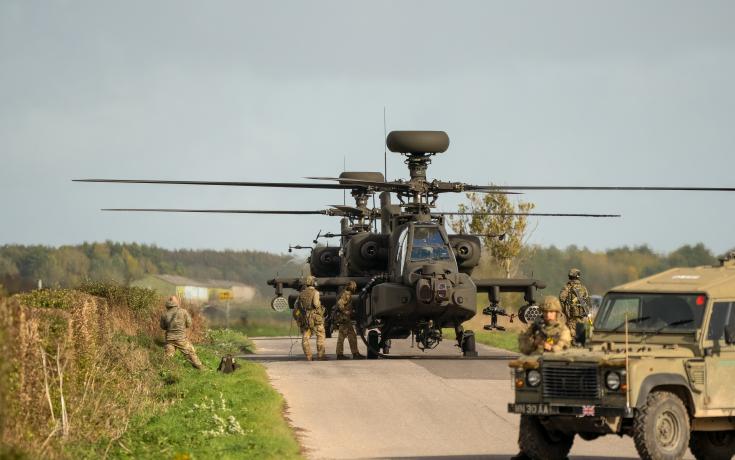
Wet blasting projects a controlled slurry of water and abrasive media on to the blade. The water cushions the abrasive on impact and is what separates this process from every alternative.
For OEM composite blade manufacture, that cushioning effect removes autoclave residues without touching the fibres beneath. What remains is a wet-out surface where adhesives, primers and coatings cover completely rather than beading, giving maximum bond area for leading edge attachment and coating application.
For MRO on metallic blades, the slurry strips paint, corrosion, grease and oils without removing substrate material. Dimensions are unchanged. Critically, the flowing slurry opens surface cracks rather than peening them closed, so blades arrive at dye penetrant or fluorescent penetrant inspection in the best possible condition for accurate defect detection. For composite blades in MRO, the process prepares surfaces for adhesive rebonding or heater mat replacement without fibre damage.
| Composite blades | Aluminium / alloy blades | Typical context | |
|---|---|---|---|
| OEM manufacturing | Surface activation after autoclaving; leading edge bonding prep | Pre-treatment before coating or anodising | High-volume, consistent blade dimensions |
| MRO / overhaul | Inspection prep; de-paint before adhesive rebond; heater mat replacement | De-paint before dye penetrant NDT; corrosion removal; recoat prep | Variable blade types and geometries between cycles |
Aluminium oxide media is used for composite blade surface preparation. Plastic media with mild detergent and hot water is used for paint stripping on metal blades without substrate damage.
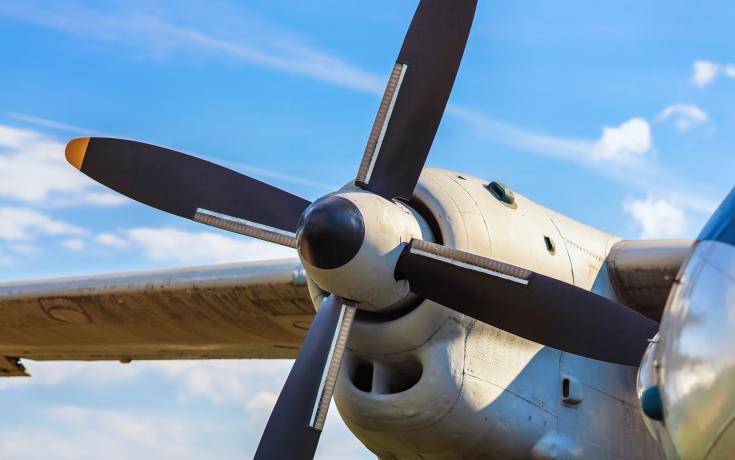
In 1982 Vapormatt delivered its first automatic machine to Westland Helicopters, to prepare composite rotor blades for bonding the metal leading edge, and it is still in operation today. Since 1978 we have supplied more than 2,000 machines to over 50 countries. There are approximately 15 measurable parameters in a wet blasting operation and Vapormatt holds multiple patents across process control, media filtration and blast gun design. The patented elutriation tower removes spent abrasive continuously without sieves, keeping media concentration consistent from the first blade to the last.
Vapormatt 4.0 records every process parameter for every component, supporting quality management traceability requirements and giving procurement and quality teams the documentation they need at audit.
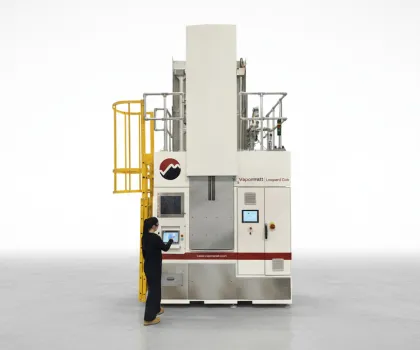
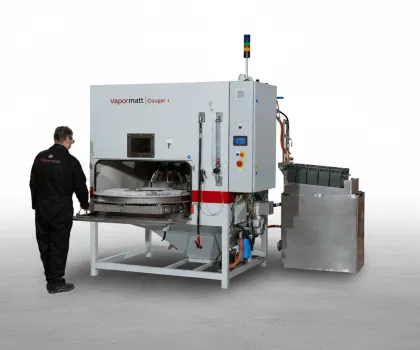
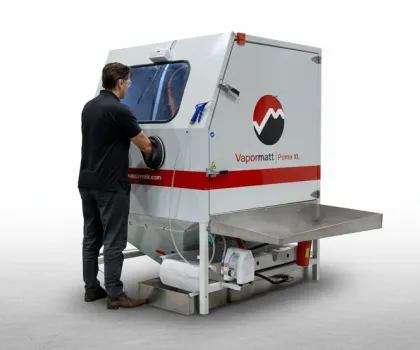
For OEM production, the Leopard Cub automatic machine processes composite propeller blades up to 2.4m (8ft) long from stored recipes. One propeller OEM replaced a manual process run by several operators with a single Leopard Cub (read the propeller blade case study, PDF). The Puma and Puma XL manual machines suit MRO shops where blade types vary between jobs, and the Cougar+ suits blade components and parts up to Ø1,200mm.
Unlike sanding, chemical stripping or dry blasting, wet blasting prepares blades in a single, controlled, recordable operation, with no operator variability, no chemical handling and no cracks closed before NDT. Composite fibres intact. Metal substrate untouched. Cracks exposed. Bond surfaces activated. Paint removed cleanly.
No. The water in the slurry cushions the abrasive on impact, so wet blasting removes surface contamination and the resin-rich layer without fracturing fibres. Within recommended parameters (up to 4 bar), no fibre damage occurs; it has only been observed above 4.5 bar. This cushioning is the key difference between wet blasting and dry blasting on composite blades.
Yes. Plastic media conforming to MIL-DTL-85891, run with mild detergent and hot water at typically 3–5 bar, lifts the paint without cutting into the aluminium. The blade comes out dimensionally unchanged. That matters for airworthiness tolerances, and for dye penetrant NDT, where the substrate must be intact.
The slurry flows across the surface and through cracks, flushing them clean rather than peening them closed. Dry blasting can close or smear over surface discontinuities and embed media in the surface. Both reduce the sensitivity of dye penetrant (DPI) and fluorescent penetrant (FPI) inspection. Wet blasting (vapor blasting) leaves cracks open and clean, so indications are easier to detect. Whether a pre-penetrant etch is still needed depends on the specification you work to.
Yes. Vapormatt 4.0 is fitted as standard to new Vapormatt machines and is available as a retrofit. It records blast pressure, slurry and abrasive concentration, and the speed of moving parts for every cycle. Customers use that record within AS9100, Nadcap, EASA Part 145 and FAA Part 43 quality systems as evidence of process control. Vapormatt also holds NATO NCAGE code U5895.
Yes. The wet blast recipe changes, not the machine. Aluminium oxide (typically 120–220 mesh at 2.5–4 bar) prepares composite blades for bonding. Plastic media with detergent and hot water strips paint from aluminium and alloy blades. A Vapormatt machine stores both recipes and switches between them, which suits mixed-fleet MRO shops.
Yes. It was the application Vapormatt’s first automatic machine was built for, at Westland Helicopters in 1982. Wet blasting removes release agents and the resin-rich surface layer without fibre damage. It leaves a surface with a 43–48° water contact angle that stays bond-ready for over two weeks. In carbon fibre testing for a major European airframe OEM, bonded joints averaged 757 J/m² fracture toughness against a 450 J/m² minimum.
Yes. Send us a blade or a representative section, with the CMM or process specification you work to. Our application engineers will process it at our UK test facility. They will return documented results covering surface condition and substrate integrity, so you can assess the finish before committing to a machine.
It depends on blade size and volume. The Leopard Cub automatic machine processes composite propeller blades up to 2.4m (8ft) long from stored recipes, and suits OEM production. The Puma and Puma XL manual machines suit MRO shops where blade types vary between jobs. The Cougar+ suits blade components and parts up to Ø1,200mm. Vapormatt also builds bespoke automatic cells.