
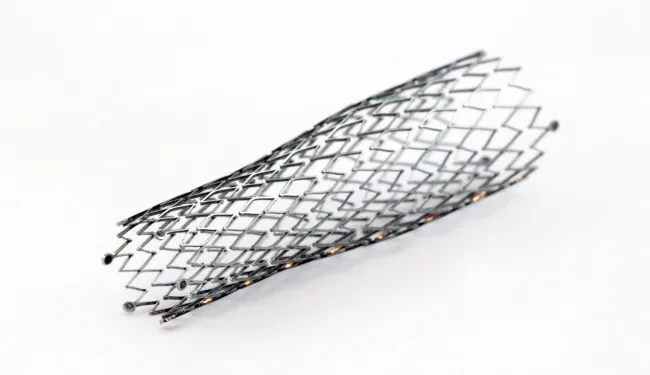
Precise
Ra tolerance consistent. Wire dimensions and transformation behaviour unchanged
Clean
Scale, black oxide, and residues removed completely. Coating-ready surface, every time
Safe
No acid baths. No HF handling. No airborne particulate
Repeatable
Every parameter stored to qualification tolerance. Batch one matches batch one thousand
Wet blasting (also called vapor blasting or vapour blasting) removes heat treatment scale, black oxide and drawing residues from Nitinol and other shape memory alloy wire in-line, without acid or dust. The Vapormatt Profelis processes continuous wire at up to 120 m/min with 360-degree blast coverage, then rinses and dries it, leaving a uniform satin finish that holds diameter tolerance and is ready for PTFE or hydrophilic coating.
If your current finishing process cannot guarantee a uniform, contamination-free surface across every metre of wire produced, you are carrying quality risk into every batch that leaves your facility. And if that process runs offline, you are absorbing a productivity cost that compounds with every production hour.
A world-leading Nitinol medical wire manufacturer runs a Profelis in-line to clean wire to the ISO and FDA standards its devices must meet.
Why traditional memory wire finishing processes are structurally limited
The dominant alternatives to wet blasting each carry a mechanism of failure that process optimisation alone cannot solve. This is true of every shape memory alloy, including Nitinol: the specific chemistry changes, but the structural problem does not.
vs. Chemical pickling and acid etching: Pickling removes heat treatment oxide, but the aggressive acid mixtures required for shape memory alloys - HF/HNO3 for Nitinol - produce microscopic changes to surface topography that create fatigue crack nucleation sites. Published research on medical-grade Nitinol confirms that pickling leaves inconsistent corrosion behaviour, with breakdown potentials varying significantly across wire samples from the same batch. The process runs offline, in acid baths, under hazardous chemical handling conditions that require dedicated containment, waste treatment infrastructure, and regulatory compliance entirely separate from your main production line.
vs. Electropolishing: Electropolishing produces a bright surface, but inclusions - the oxides, carbides and oxidised carbides present in the bulk microstructure of Nitinol and other shape memory alloys - are retained on the electropolished surface. Corrosion initiates around those inclusions in service environments. In process trials on medical-grade Nitinol wires show that electropolished samples can exhibit lower breakdown potentials than chemically treated equivalents precisely because of this mechanism. Electropolishing also requires pre-treatment deoxidation, a controlled electrolyte, and temperature management. It is a batch process. It does not integrate with continuous wire production at line speed.
vs. Dry blasting: Dry blasting is widely used for scale removal but is demonstrably ineffective for memory wire finishing. Process trials confirm that dry sandblasting does not achieve complete oxide removal from the original scaling on Nitinol, and subsequent drawing compounds the problem by creating a persistent scale layer.
Each of these processes was developed for different applications and adapted for memory wire. None was designed for it.
Find out how wet blasting compares with other finishing processes
Wet blasting applications for memory wire manufacturing
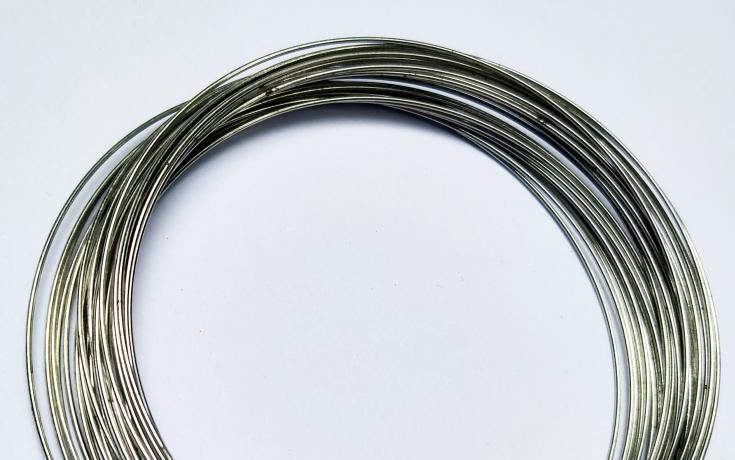
Wet blasting removes heat treatment scale, oxides and manufacturing residues from memory wire while holding it within its diameter tolerance and leaving its transformation temperature behaviour unchanged. This applies equally to Nitinol, copper-zinc-aluminium, iron-manganese-silicon and other shape memory alloy wire products. The water-cushioned abrasive delivery avoids the surface stress introduction associated with dry blasting, and the closed-loop slurry system eliminates the airborne dust and static build-up that make dry blasting unsuitable for precision wire manufacturing environments. Where a target diameter is needed, a different recipe removes substrate in a controlled way to bring the full length of wire to a consistent diameter.
The result is a uniform, satin-like finish with controlled surface roughness: clean, reactive, and consistent across the full length of the wire - including every metre processed through a continuous inline system.
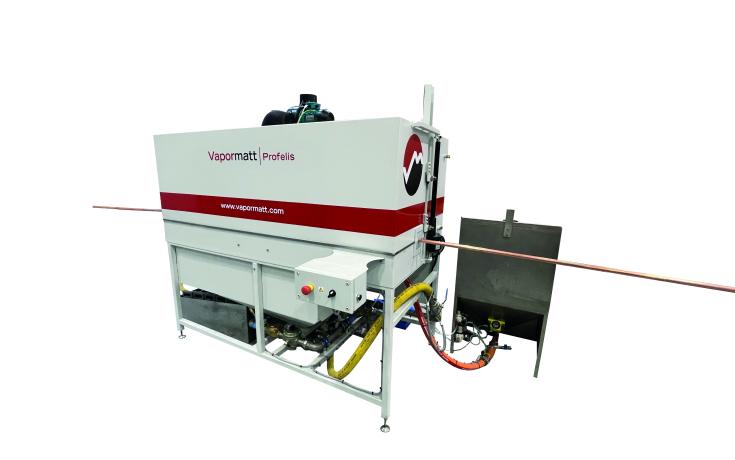
Wet blasting memory wire in the Profelis - key facts:
| Parameter | Value |
|---|---|
| Alloys | Nitinol (NiTi), copper-zinc-aluminium, copper-aluminium-nickel, iron-manganese-silicon |
| Wire diameter | From 1mm (0.04") (see item 18) |
| Line speed | Up to 120 m/min (394 ft/min), depending on diameter, alloy and finish |
| Coverage | 360 degrees: 4 guns at 90° as standard, 8 guns at 45° optional |
| After blasting | In-line rinse and air wipe; vacuum drying optional |
| Process control | Named recipes stored on the HMI; patented flow control |
| Finish | Uniform satin finish with controlled Ra |
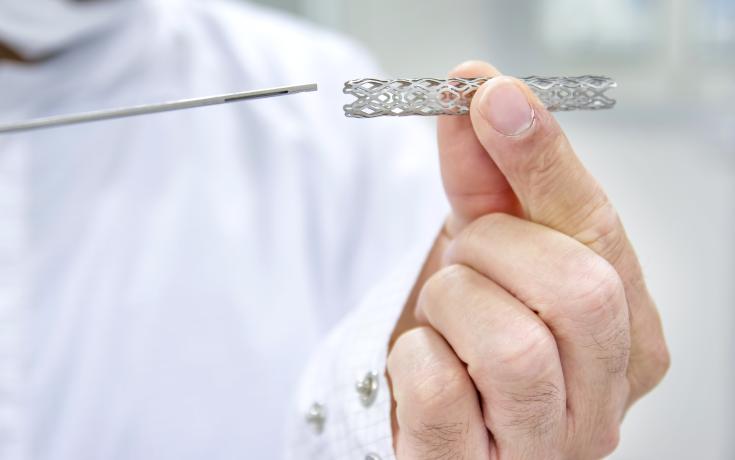
Specific applications handled include:
- Heat treatment scale and black oxide removal from shape-set Nitinol wire, flat wire, and ribbon
- Oxide removal from copper-zinc-aluminium and copper-aluminium-nickel memory wire after annealing
- Uniform surface preparation for PTFE and hydrophilic coating adhesion on Nitinol guidewires
- Controlled surface texture for Nitinol braiding wire used in self-expanding vascular stents
- Cleaning of Nitinol orthodontic arch wires prior to functional testing and packaging
- Controlled removal of substrate to achieve a uniform wire diameter
- Surface preparation of iron-based shape memory alloy wire for structural and civil engineering applications
- Oxide and residue removal for Nitinol IVC filters, clot retrievers, and flow diverters
- Finishing of memory wire for actuator, robotics, and industrial SMA applications
- Surface preparation of Nitinol and copper-based wire for wearable device and MEMS components
Why Vapormatt
Vapormatt is the originator of the wet blasting machine and the only wet blasting company to have developed a dedicated inline machine for continuous wire and cable processing. That depth of process engineering is visible in how the Profelis performs at production scale across the full range of memory wire alloys.
For Nitinol wire manufacturers supplying material conforming to ASTM F2063 and operating within ISO 13485 quality management frameworks, that level of repeatability is a compliance requirement, not a commercial advantage.
The bottom line
Memory wire - whether Nitinol for cardiovascular devices, copper-zinc-aluminium for industrial actuators, or iron-based alloys for structural applications - demands a finishing process that removes contamination completely, preserves dimensional accuracy, maintains fatigue integrity, and repeats that outcome across every metre of production. Chemical pickling carries fatigue risk. Electropolishing is constrained by inclusion behaviour and batch processing limits. Dry blasting cannot achieve complete oxide removal. Wet blasting, delivered inline via the Profelis, solves all three in a single continuous process step.
Every batch that leaves your facility without a verified, repeatable surface finish carries quality risk that accumulates. The audit finding, the rejected lot, the delayed device submission or the failed actuator specification: the cost of doing nothing is not abstract.
Related machines
FAQs
What types of memory wire can wet blasting finish?
The Vapormatt Profelis in-line wet blasting machine processes shape memory alloy wire including Nitinol (nickel-titanium), copper-zinc-aluminium, copper-aluminium-nickel and iron-manganese-silicon, from 1mm diameter upwards. Each alloy requires specific process parameters - blast pressure, media type and line speed - which are set at qualification, stored as a named recipe and recalled at the touch of a button.
Does wet blasting affect the super elastic or shape memory properties of the wire?
No. Wet blasting removes surface contamination without the material-aggressive chemistry of acid pickling or the electrochemical process complexity of electropolishing. The water-cushioned abrasive delivery minimises surface stress introduction, preserving the fatigue life and transformation behaviour engineered into the wire through prior thermomechanical processing - for Nitinol, copper-based, and iron-based alloys alike.
How does wet blasting compare to chemical pickling for memory wire oxide removal?
Chemical pickling removes oxide but introduces microscopic surface topography changes that create fatigue nucleation sites - a documented risk for any wire used in cyclic-load applications. Wet blasting removes scale with a water-cushioned abrasive, without fatigue risk, without an acid waste stream, and without the offline processing constraint. The Profelis runs inline with your production at line speed.
Is the wet blasting process compatible with ISO 13485 and ASTM F2063 manufacturing environments?
Yes. The Profelis delivers fully programmable, repeatable process parameters with HMI recipe storage and consistent blast gun output maintained through Vapormatt's patented flow control technology. This level of documented process control supports the validation and batch traceability requirements of ISO 13485-certified medical device manufacturing and supply chains producing Nitinol conforming to ASTM F2063.
Is wet blasting safe for use in a precision wire manufacturing environment?
Wet blasting suppresses airborne dust by suspending abrasive media in water, eliminating the particulate exposure associated with dry blasting. It eliminates the static build-up that dry processes generate around fine wire. There are no acid baths, no Hydrofluoric acid handling requirements, and no acid waste treatment infrastructure required. For a cleanroom-adjacent, ISO-classified, or sensitive industrial manufacturing environment, wet blasting is the operationally and environmentally safer process choice.
What diameter of memory wire can be wet blasted?
The Vapormatt Profelis processes continuous wire from 1mm up to 54mm (2.13"). Fine wire can be run as several strands at once using Vapormatt’s patented micro nozzle configuration.
How fast can memory wire be wet blasted in-line?
The Profelis runs at up to 120 m/min (394 ft/min). Actual speed depends on wire diameter, alloy and the finish required, and is set as part of the qualified recipe. The wire is rinsed and dried in the same pass, so it leaves the machine ready for the next production stage.
Is wet blasting the same as vapor blasting?
Yes. Wet blasting, vapor blasting, vapour blasting and slurry blasting all describe the same process: fine abrasive suspended in water and blasted onto the surface. The water cushions the abrasive, so it cleans without embedding media and suppresses dust.
Can I trial wet blasting on my own Nitinol wire before buying?
Yes. Send a sample of your wire to Vapormatt’s sample processing facility. It is processed to a recipe developed for your alloy and diameter, and returned with a full test report covering the recipe, measurements and photographs.
Contact us to organise sample processing