Image

Degrease, de-paint, and prep for inspection in one pass.
No media embeds. No masked discontinuities. NDT you can trust
No solvents. No dust. No hydrogen embrittlement risk
Every component finished identically and fully documented
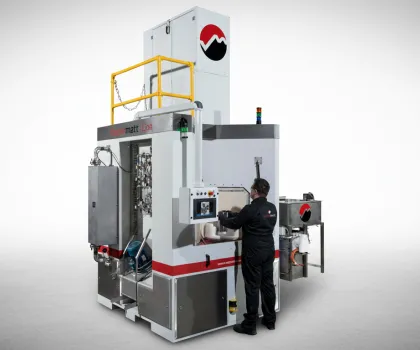
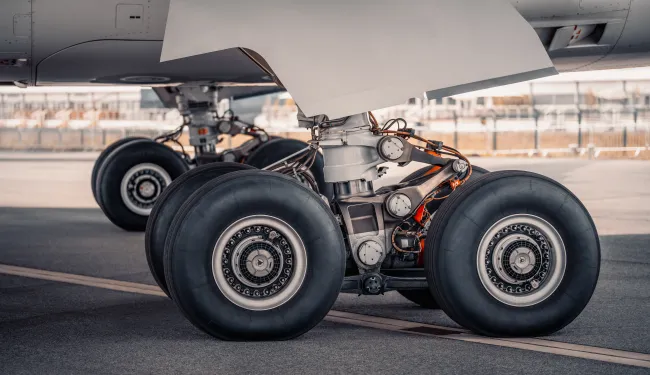
Wet blasting (also called vapor blasting) prepares aircraft landing gear for NDT and recoating by stripping paint, removing grease, Skydrol and heat scale, and conditioning the surface in one controlled pass, without embedding media or using solvents.
Every undercarriage component that enters your overhaul shop carries a compliance obligation, a turnaround deadline, and a safety risk. Get the surface preparation wrong and the NDT result is unreliable. Take too long and your TAT commitment is compromised. Use the wrong method and you risk hydrogen embrittlement in high-strength steel, media contamination in threaded features, or coating adhesion failure after repainting.
Wet blasting replaces three sequential surface preparation operations (paint stripping, degreasing, and surface conditioning) with a single controlled pass. That reduction in cycle steps is where turnaround time is recovered and process variability is eliminated.
Vapormatt has supplied wet blasting machines to aerospace MRO operations since the late 1940s. That origin means more proven process generations, more OEM-specific parameters developed, and more documented outcomes than any competitor entering this industry later. For undercarriage MRO, that depth matters.
vs. solvent and chemical cleaning: Landing gear components arrive coated in compacted contamination: asphalt deposits, Skydrol, brake dust, hydraulic fluid, and layered paint systems. Chemical degreasers remove surface oils, but they are single-function. Paint removal requires a separate sequential operation, each step adding handling time and documented process control requirements. Several common solvents, including trichloroethylene (TCE) and n-propyl bromide (nPB), carry serious occupational health risks, face tightening regulatory controls, and can cause hydrogen embrittlement in high-strength steel struts and torque links if process discipline lapses. The disposal and compliance burden of chemical cleaning is one that MRO operators are increasingly unable to justify.
vs. dry blasting: Dry blasting removes scale and paint at speed, but introduces risks that are difficult to manage on safety-critical components. Media particles can embed in the surface substrate, filling micro-discontinuities that dye penetrant inspection (DPI) and eddy current testing (ECT) must later reveal, producing false-negative NDT results. On ferrous components, dry blast media generates charged particles and dust that present static hazards. The accuracy cost of pre-NDT dry blasting is invisible until it isn’t.
vs. manual hand scrubbing and chemical paint stripping: Manual preparation relies entirely on operator skill, is inconsistent part-to-part, and is time-consuming at scale. Documented repeatability, a core requirement of regulated MRO, is difficult to achieve and audit-prove with manual methods. Wet blasting automates and records all critical parameters, producing a surface that is consistent and traceable.
Find out how wet blasting compares with other finishing processes
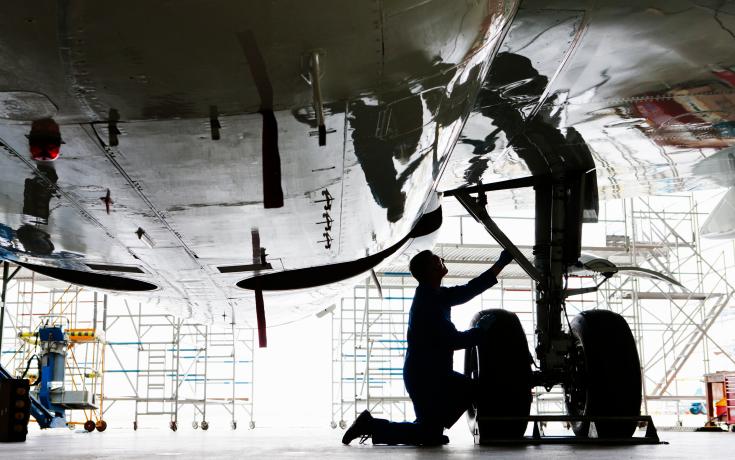
Three outcomes are consistently achieved in a single operation: paint stripping, degreasing, and surface conditioning for inspection or re-coating. Three sequential operations become one. Cycle time falls. Documented repeatability rises.
The mechanism is specific. Water-borne abrasive slurry is accelerated through a nozzle onto the component surface. The water acts as a lubricant and cushion, flowing over complex geometries (including threads, bores, and recessed fittings) while the abrasive removes contaminants. Because the abrasive is carried in liquid rather than air alone, media does not embed in the surface. Discontinuities remain open and visible. The surface is left clean, consistent, and ready for accurate NDT.
Up to 15 independent parameters govern the wet blasting operation: nozzle pressure, slurry concentration, media type, media size, blast angle, blast distance, water temperature, cycle time, and others. Vapormatt’s engineering and automation systems control all of them. Every part processed on the same programme receives an identical surface, and that consistency is the difference between a process that passes audit and one that doesn’t.
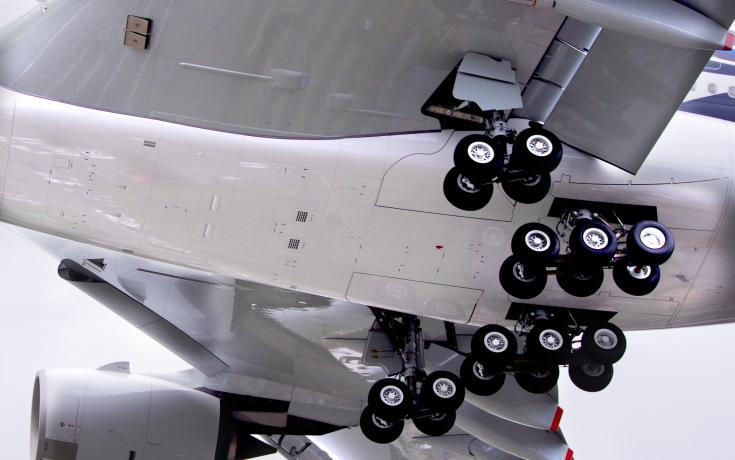
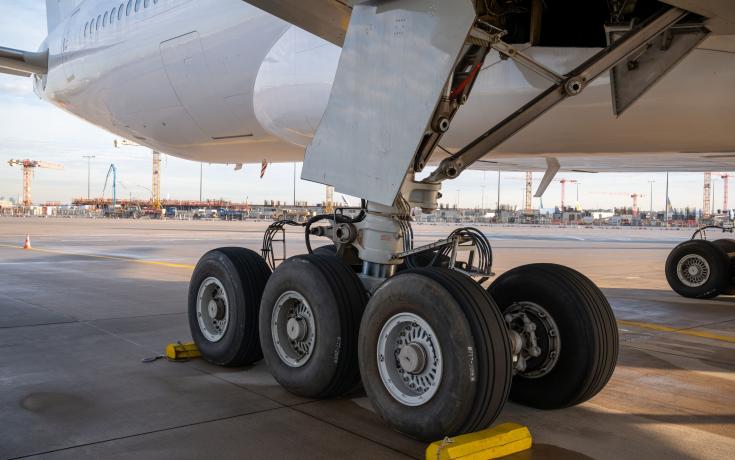
Wet blasting handles the full scope of undercarriage component preparation across the overhaul cycle:
Vapormatt has been developing wet blasting parameters for aerospace-grade components for longer than any other machine supplier in the market. That means more material-specific process data, more OEM-approved parameters on record, and more application engineers who have worked within EASA and FAA-regulated environments.
Vapormatt machines are used by leading aerospace MRO organisations globally. The company holds NATO NCAGE code U5895, relevant to both civil and military aerospace operations, confirming its status as an approved supplier to defence and aerospace programmes worldwide.
For cadmium-plated fixings and fasteners, wet blasting with correctly specified media and parameters cleans and prepares the surface without stripping the sacrificial coating that protects against corrosion in service.
The MRO process that returns landing gear components to service must be fast, repeatable, and fully auditable. Wet blasting (vapor blasting) replaces three sequential surface preparation operations with one controlled process, reducing turnaround time, eliminating solvent handling risk, and producing surface conditions that give NDT inspectors accurate, reliable results. In comparable aerospace NDT preparation, Vapormatt customers have cut A350 wheel-half stripping from 120 to 58 minutes and total compressor-hub preparation from 430 to 88 hours.
The alternative is multi-stage preparation, variable outcomes, escalating chemical compliance costs, and a process that is difficult to document to the standard your quality system demands.
Wet blasting removes all surface contamination, including oils, paint, and scale, without embedding media in the surface. Because discontinuities remain open and unobstructed, DPI penetrant seeps in fully and ECT signals are not masked by residual contamination. Dry blasting carries the risk of closing discontinuities with embedded media particles, which can produce false-negative results on safety-critical components.
Wet blasting is an entirely documentable, repeatable process. Vapormatt’s automated machines operate to programmed parameter sets, meaning every component processed receives an identical, traceable surface preparation. This supports the process control and documentation requirements of EASA Part 145 and FAA Part 43 quality management systems. Vapormatt holds NATO NCAGE code U5895 and supplies MRO organisations operating under both regulatory frameworks.
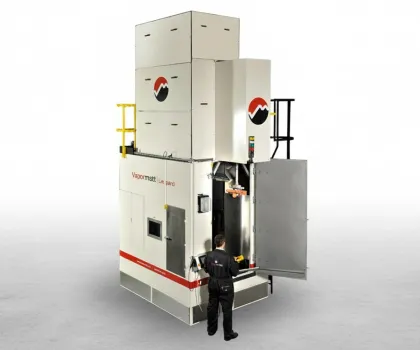
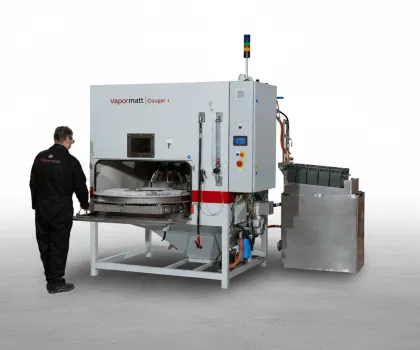
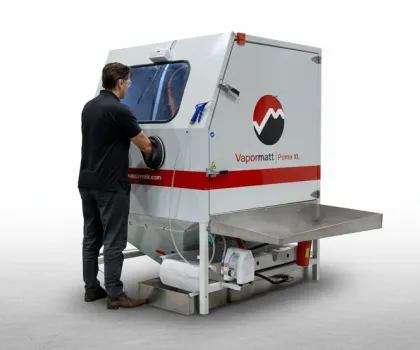
Yes. Vapormatt’s range includes manual machines suited to low-volume, high-complexity components, and automated and robotic machines for higher throughput. For large structural components such as main gear struts, machines with overhead crane loading access and programmable nozzle manipulation process parts that manual methods cannot handle consistently. For smaller components including fixings, barrel-configured machines process in volume without manual handling of individual parts.
Yes. Send us representative parts, such as a strut, actuator or torque link, and our applications engineers will process them at our R&D facility in Bridgwater. You get the parts back with the recommended media, parameters and machine, so you can check the result against your NDT and coating requirements before you commit.
Yes, and this is a meaningful operational advantage. Because the abrasive is carried in water, titanium particles are wetted and contained within the slurry rather than becoming airborne. This suppresses the static charge and dust risk that makes dry blasting of titanium subject to ATEX requirements. Wet blasting eliminates that compliance overhead entirely.
No. A rust inhibitor can be added to the wet blast slurry mix by controlled dosing. Parts leave the machine dry and ready for NDT or primer, which is why wet blasting is used on high-strength steels such as 300M and 4340.