Wet blasting for continuous rotary extrusion...
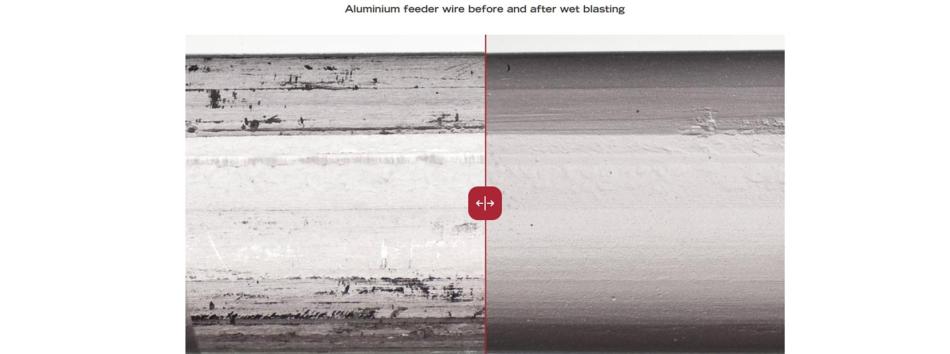
Most continous rotary extrusion (CRE) operators assume inconsistent output is a feedstock problem. More often, it's a surface preparation problem.
CRE is unforgiving. The wheel grips rod by friction alone, and any oxide layer, scale, or residual lubricant carried into the groove gets pulled through into the extruded product, where it causes porosity, blister defects, and conductivity loss. There is no correcting it downstream.
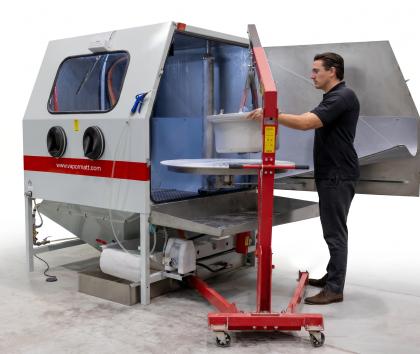
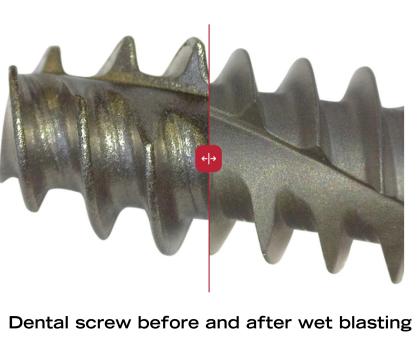
Our Profelis automatic Wet blasting machine removes oxides, scale, and lubricants uniformly across the full 360-degree rod surface, without embedding media or altering dimensions. Integrated rinsing and drying mean the rod enters the extrusion zone clean and ready, with no additional handling.
The result: stable line speeds up to 30 m/min, fewer stoppages, and the freedom to run lower-grade feedstock, including rod stored outdoors, without compromising output quality.
Learn more about wet blasting for continuous rotary extrusion