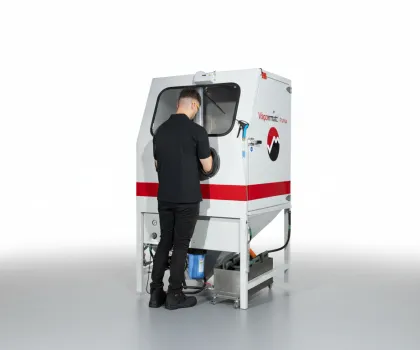
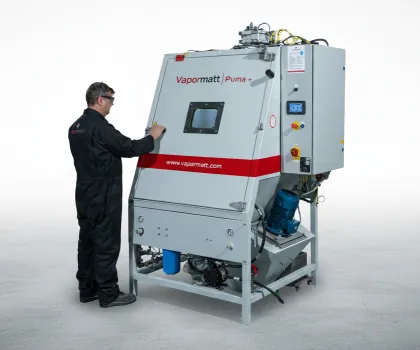
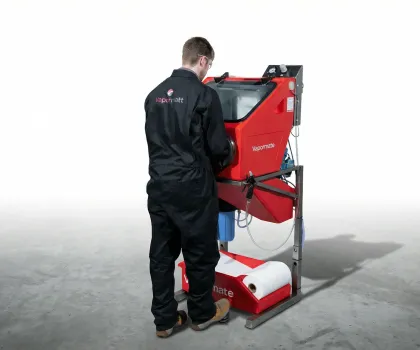
Image

Wet blasting (also called vapor blasting or vapour blasting) is a post-processing method for 3D printed metal and polymer parts. In a single dust-free, chemical-free operation, it depowders complex internal channels, reduces Ra on metal parts from a typical 15–20 µm to below 1.6 µm, and converts tensile surface stresses to compressive, improving fatigue life.
If you'd rather discuss your specific finishing requirements or request sample processing of your components, speak to one our experts.
No airborne dust and no hazardous chemicals, for a safer, simpler process
Precise, independently adjustable Ra to specification across complex geometry, inc. internal features
Powder removal, surface finishing, and coating prep - done in one operation
Proven across the main AM materials: titanium, Inconel®, aluminium, polymers, composites
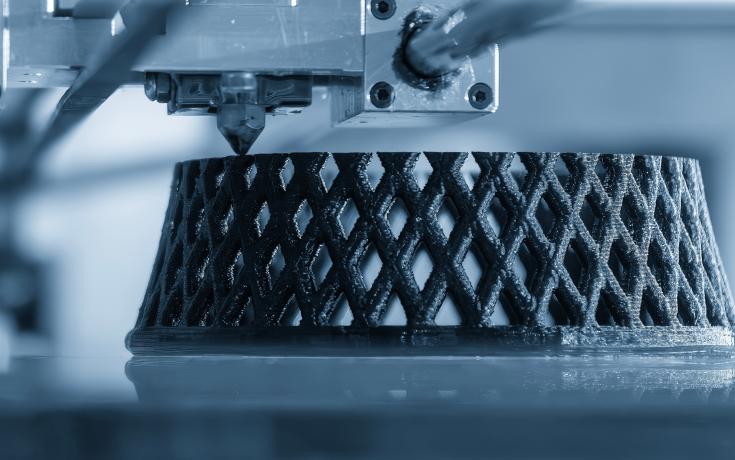
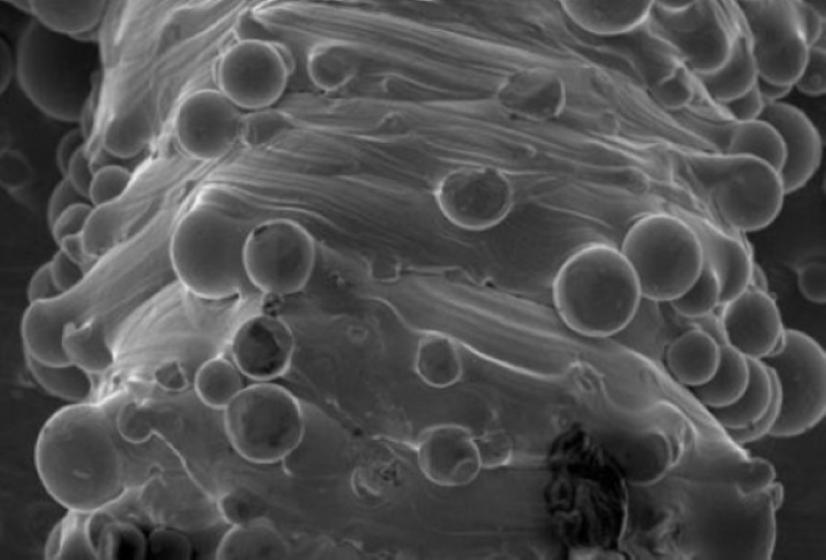
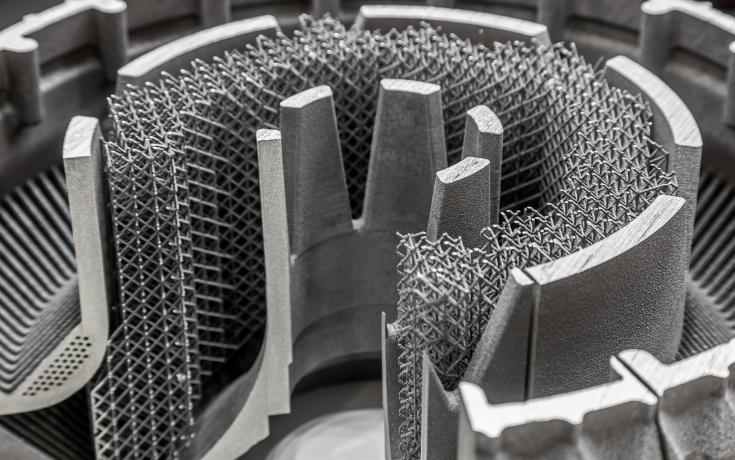
Your 3D printer delivers a near ideal looking component. Then reality arrives. Layer lines visible to the naked eye. Residual and partially sintered powder locked inside channels too complex to brush clear. Tensile stresses built into the surface by the thermal cycling of the build process. An as-built Ra of typically 15 to 20 microns on a DMLS metal part where your specification demands 1.6 or below.
Post-processing is not an afterthought in additive manufacturing. It's where the value of the print is either realised or lost. The wrong finishing process damages the geometry you just paid to build. The right one transforms an as-printed part into a production-quality component, in a single operation.
3D printed metal parts or 3D printed polymer parts carry three properties that make conventional finishing unsuitable: extreme geometric complexity, delicate surface tolerances, and the presence of un-sintered or partially sintered powder. Each of these demands a process with genuine finesse.
| Wet blasting | Dry blasting | Chemical / electrochemical polishing | Mass finishing (vibratory / tumble) | Vapor smoothing | |
|---|---|---|---|---|---|
| Clears powder from internal channels | Yes, with visible confirmation | Unreliable; can compact powder further | Difficult to verify | No | No |
| Controlled Ra to specification | Yes, adjustable per part | Limited control | Yes, on external surfaces | Yes, on simple external shapes | Smooths, but Ra is not adjustable |
| Targets specific areas | Yes | Yes | No | No | No |
| Adds compressive stress (fatigue life) | Yes | Yes | No | No | No |
| Dust or explosion risk | None; powder held in water | High, especially with titanium | None | Low | None |
| Hazardous chemicals | None | None | Yes | Compounds only | Yes, solvents |
| Risk of media embedment or part damage | Low; water cushions impact | High | Low | Part-on-part contact damage | Low |
| Materials | Metal and polymer | Metal and polymer | Mainly metal | Metal and polymer | Polymer only |
| Depowders, finishes and preps for coating in one step | Yes | No | No | No | No |
Find out how wet blasting compares with other finishing processes
Wet blasting, otherwise known as vapor blasting or aqua blasting, addresses the finishing challenges that matter most in AM production, in a single controlled operation. Few processes deliver all three in a single operation: a finish that can remove the need for a separate CNC finishing step, thorough powder removal with visible confirmation that each channel is clear and flowing, and compressive stress that improves fatigue life.
The mechanism is precise. A slurry of water and abrasive media is delivered under controlled pressure through calibrated blast guns. The water cushions the impact, protecting delicate surfaces while the abrasive acts. Media concentration, air pressure, nozzle angle, and dwell time are each independently controllable, delivering a specific Ra to specification across the entire component surface - including recesses and internal features that line-of-sight processes struggle to reach.
The clearest proof of channel clearance is built into the process itself. When wet blast slurry exits a cleared internal channel, it is visible. Dry blasting offers no equivalent visual confirmation.
SLS polymer parts · Vapormatt Puma
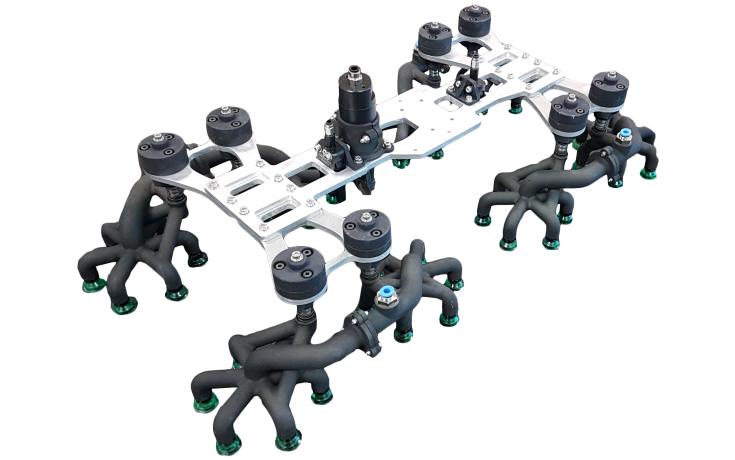
Challenge: Anubis 3D's vacuum gripper for autonomous grocery stores relies on complex internal channels that must be completely free of powder. Dry blasting couldn't clear them reliably, so powder removal was a hit and miss affair, and airborne powder created an explosion risk.
Result: The Puma now removes all trapped powder, and the slurry flowing out of each channel confirms it is clear. It also produces a better finish than dry blasting, with no dust risk.
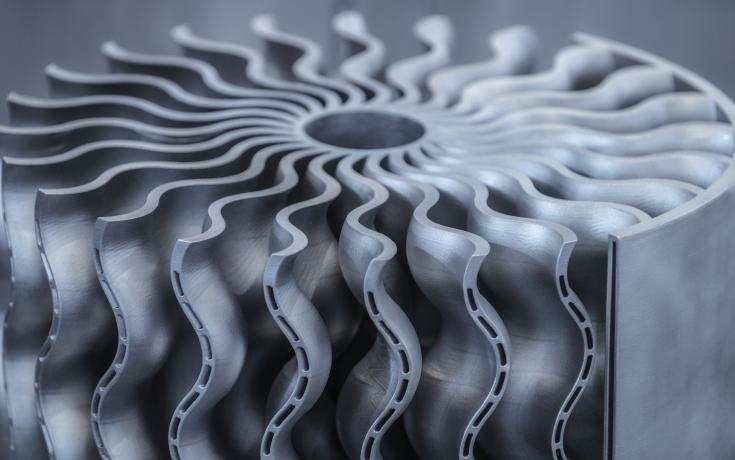
Additive manufactured aerospace, dental and medical components are finished using our wet blast technology.
Learn more about wet blasting for aerospace
Learn more about wet blasting for dental and medical implants
From our Anubis 3D case study: The Vapormatt Puma wet blasting machine allows the complete removal of trapped sintered powder from complex internal channels. It also achieves a higher-quality surface finish on SLS additive manufactured components compared with dry blasting, whilst eliminating the explosion risks associated with airborne powder.
We saw a significant improvement in fatigue lives at 0.003 and 0.0025 mm/mm, attributed to very high compressive residual stress at the surface layer.
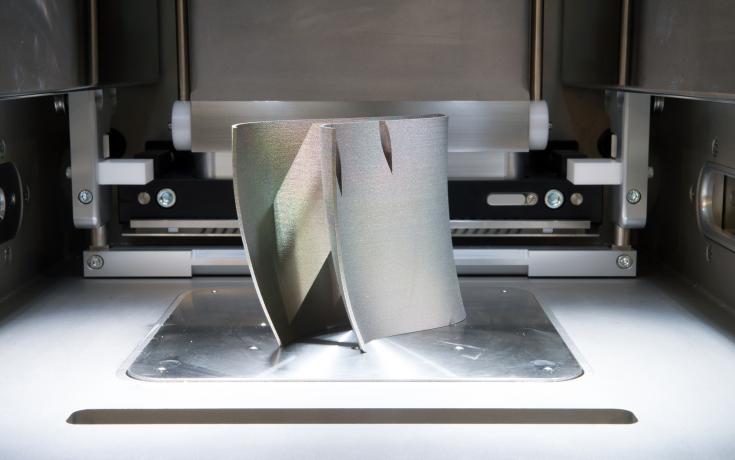
The case for Vapormatt rests on three things: the depth of process knowledge behind the machines, the precision of the machines themselves, and a track record of installation across AM's most demanding applications.
A UK based DMLS facility specialising in titanium components for aerospace and medical, reviewed multiple finishing suppliers before selecting Vapormatt. The Vapormate is now an integral part of their production process, finishing parts within minutes of build completion and eliminating the titanium combustion risk that ruled out dry blasting as an option.
Vapormatt machines are built for industrial longevity. We still service machines manufactured in the 1980s. For an AM operation scaling to production volumes, that matters: the finishing process must keep pace with the printer, and not require replacing every five years.
The process control that makes this possible is protected by Vapormatt patents, granted in 22 countries between 1982 and 2021. Consistent slurry delivery from blast guns, media filtration and recirculation, and Vapormatt 4.0 digital process monitoring are not generic wet blasting features - they are Vapormatt-specific developments, refined over decades of installation in aerospace, medical, and defence environments where repeatability is not optional.
Additive manufacturing / 3D printing unlocks geometry that traditional manufacturing cannot achieve. Wet blasting is the finishing process that makes that geometry functional. It depowders, controls Ra to specification, converts tensile surface stresses to compressive, prepares surfaces for coating adhesion, and does all of this without chemical hazards or airborne dust, with the water cushion protecting delicate features and fine detail.
The cost of getting this wrong is not just a rejected part. It is a failed coating, a cracked component in service, a channel that never passed inspection, a batch processed without knowing whether it was finished to specification. Vapormatt invented wet blasting in the late 1940s and has developed it ever since, including for AM. The machines exist. The R&D capability exists. The track record exists.
Yes. The wet blast slurry is a pressurised liquid, which means it flows into and through complex internal channels rather than compacting material within them. When the slurry exits the channel, it is visible - providing a direct, physical confirmation that the channel is clear. This is a reliable and repeatable method of depowdering that dry blasting and chemical processes cannot replicate with the same confidence.
Wet blasting suits titanium because the abrasive and the removed material stay suspended in water, so no combustible dust cloud forms and there is no static discharge to ignite one. Dry blasting titanium requires explosion-protected equipment and strict controls. Fines collected by the filtration system should be kept wet and disposed of in line with NFPA 484 or your local requirements: see our guide to health and safety in wet blasting.
This depends on the material, the AM process, and the media selected. DMLS metal parts typically have as-printed Ra values of 15 to 20 microns. Wet blasting can reduce surface roughness significantly and achieve Ra values below 1.6 microns on metal AM components. Vapormatt's R&D facility, equipped with an Alicona surface measurement system, can quantify achievable Ra values on your specific material and geometry through a sample processing programme before machine investment.
Yes. Vapormatt machines are in daily use at aerospace OEMs and medical implant manufacturers operating under AS9100, ISO 13485 and customer-specific specifications. The machine supports your validated process: repeatable slurry delivery and Vapormatt 4.0 digital monitoring give you the documented process data an audit requires. Certification remains yours, against your own process.
Yes. Wet blasting can complete powder removal, surface finishing to a target Ra, and surface preparation for coating or bonding in a single operation. For AM tools or components requiring both surface finishing and coating pre-treatment, this multi-stage capability reduces handling time, eliminates transfer between separate processes, and lowers the risk of inter-process contamination.
No. Vapor blasting (wet blasting) is a mechanical process: a slurry of water and abrasive media cleans, depowders and finishes the part. Vapor smoothing is a chemical process: solvent vapour melts and reflows the outer surface of polymer parts such as SLS or MJF nylon. Vapor smoothing works on polymers only, doesn't clear powder from internal channels and adds no compressive stress. Wet blasting works on both metal and polymer AM parts. It's often used before vapor smoothing so the part goes in clean and powder-free.
Wet blasting removes very little material. The water cushions each impact, so it smooths layer lines and partially sintered particles without eroding edges or fine features. Pressure, media type, concentration and dwell time are all adjustable, so material removal can be kept within your tolerance. For critical dimensions, a sample processing trial will measure the effect on your own parts before you commit.
No. Supports still need to come off by cutting, machining or wire EDM, as they do today. Once the supports are removed, wet blasting blends the witness marks they leave, clears any remaining powder and brings the whole surface to a consistent finish in the same operation.
It depends on the part's size and complexity, the material, the starting roughness and your target Ra. Simple parts can take minutes. Complex parts with long internal channels take longer, because every channel must run clear. A sample processing trial on your own parts will give you real cycle times to base your production planning and ROI on.
Media choice depends on your material and the finish you need, and Vapormatt machines run all the common types without modification. As general starting points:
The best choice for your parts is confirmed during a sample processing trial.
Yes. Manual machines such as the Vapormate and Puma suit R&D, trials and lower volumes. The Puma+ automatic machine delivers consistent, repeatable batch processing, with a barrel option for tumbling batches of small polymer parts. Parameters proven on a manual machine transfer directly to automatic production, and Vapormatt 4.0 digital monitoring records the process data regulated industries need.
Vapormatt machines use a closed-loop system as standard. Filtration captures removed powder and worn media, while good media and the water are recirculated. Because the powder is held in water, it never becomes airborne. Collected residue should be handled according to your material's safety requirements, particularly reactive metal fines such as titanium. See our health and safety guide for more.
Cost depends on the machine size, the level of automation and your options, so we quote for your specific application. Payback typically comes from:
Dry blasting delivers force without control. The absence of water means no cushioning effect, no lubrication between media and surface, and a genuine risk of media embedment in the component. On titanium, it carries an additional hazard. Fine titanium powder is a combustible dust, and dry blasting generates both the airborne cloud and the static discharge that can ignite it. It can be done safely, but only with explosion-protected equipment and strict controls under standards such as NFPA 484, DSEAR and ATEX, which add cost and complexity. Dry blasting also struggles to clear internal channels reliably. In our Anubis 3D case study, dry blast residue settled on top of powder already trapped inside the channels. It is possible to compact loose powder further into a channel rather than remove it, creating a blockage with no visible indication of the problem.
These processes can achieve low Ra values on external surfaces. Treating specific surface regions selectively requires masking, which adds cost and process steps. They require hazardous chemistry and the associated handling, storage, and disposal costs, and they provide no compressive stress benefit. For parts with complex internal geometry, uniformity of treatment is difficult to verify and difficult to achieve.
Effective for simple external geometries and batch processing of small polymer parts. The media flow cannot reliably reach and treat complex internal channels. It delivers no controlled, measurable peening intensity. And for high-value, low-volume metal components, batch processing introduces the risk of part-on-part contact damage.
Note: Inconel is a registered trademark of Special Metals Corporation.