
Technical challenge: large components, tight tolerances, variable workloads
Large aerospace components combine three demands that general-purpose blast machines handle poorly. Large, complex shapes need uniform coverage across every surface. Engine Standard Practices Manuals (SPMs) and AMS 2432 peening need real-time process monitoring, with an alarm or shutdown on any deviation. And MRO workloads are low-volume and high-variance, so the machine must switch between component profiles quickly. A machine that also needs a pit or other civil works before it can be installed is expensive before it processes a single part.
Two configurations for the full range of large-format components
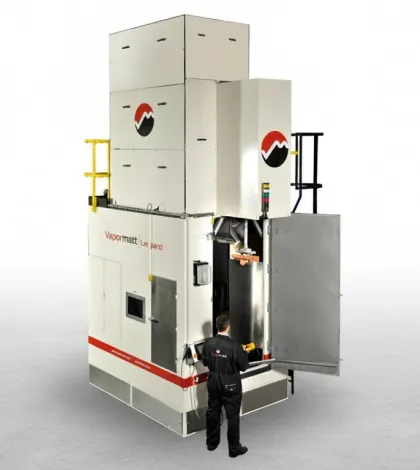
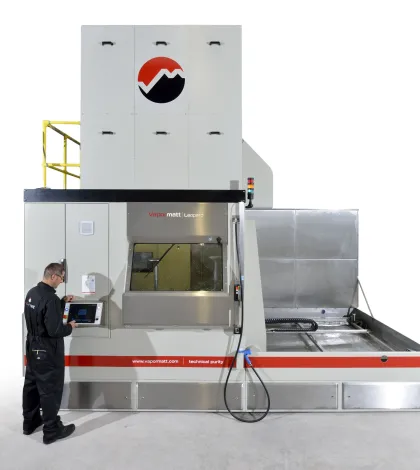
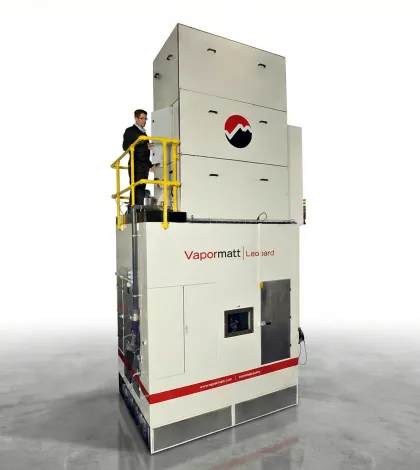
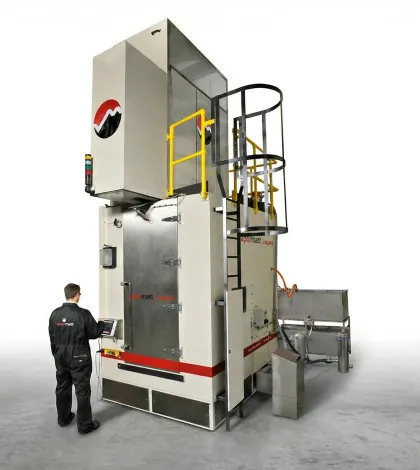
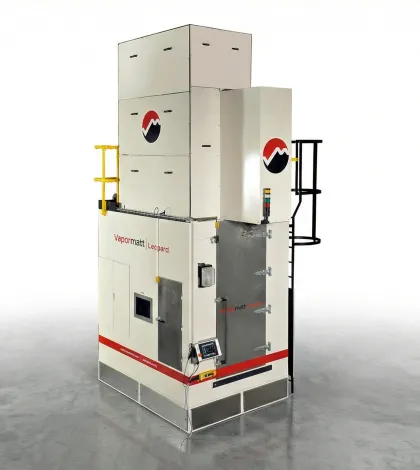
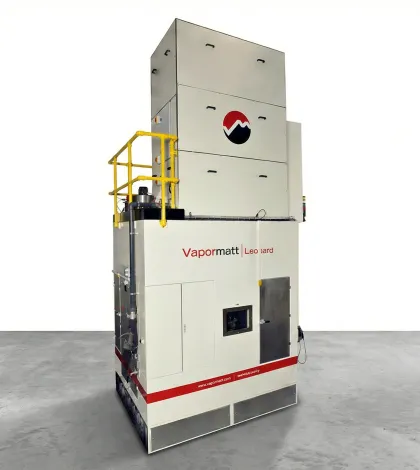
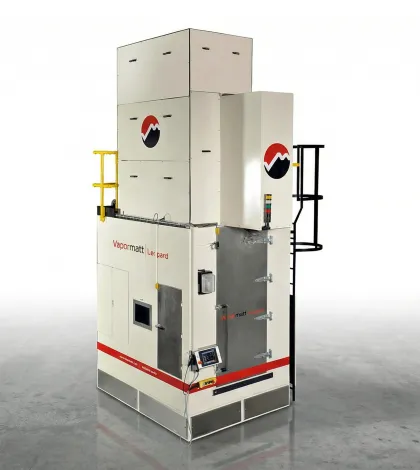
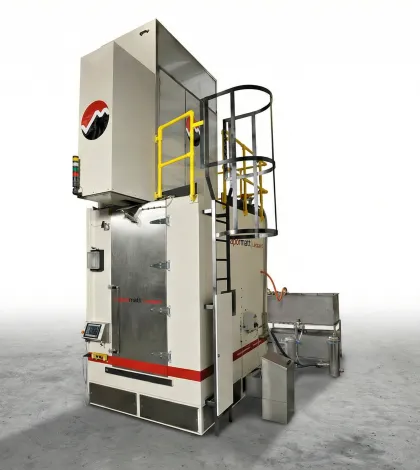
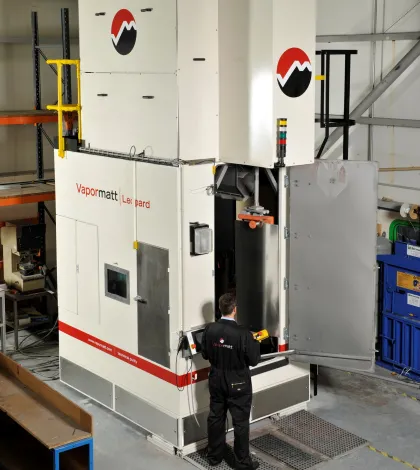
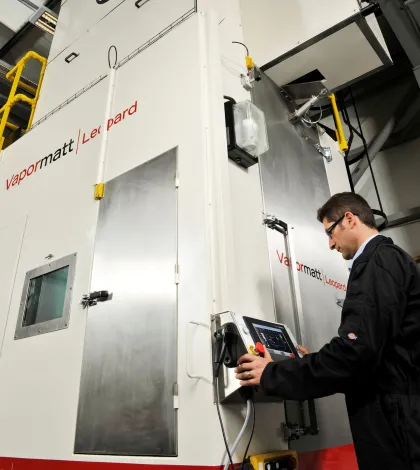
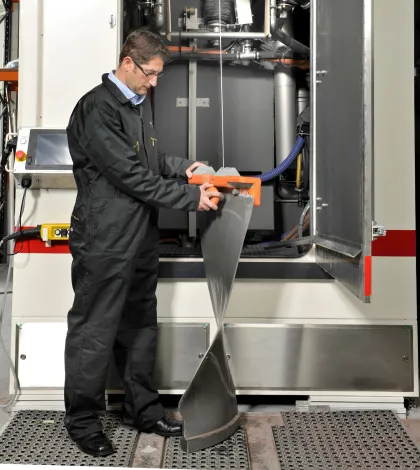
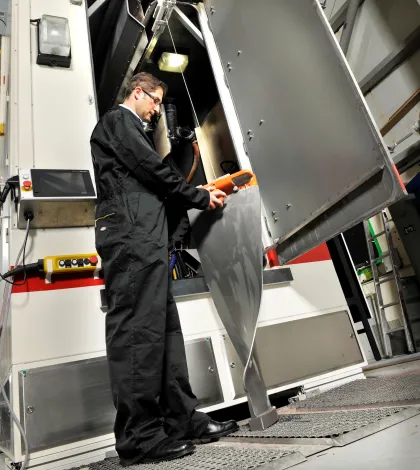
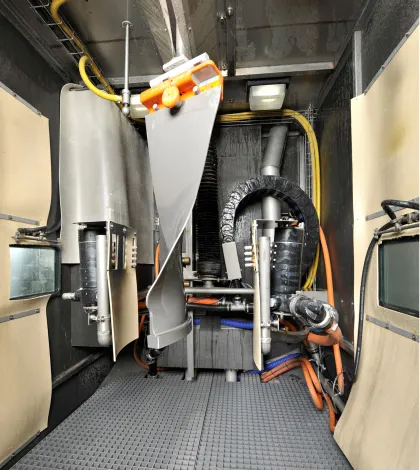
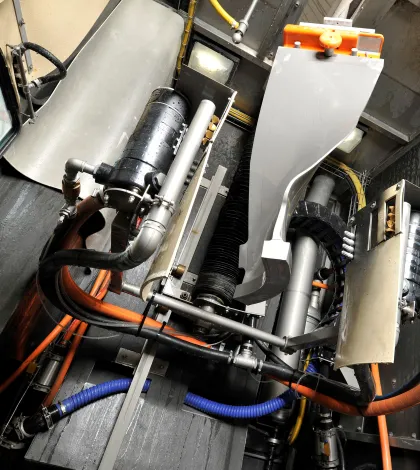
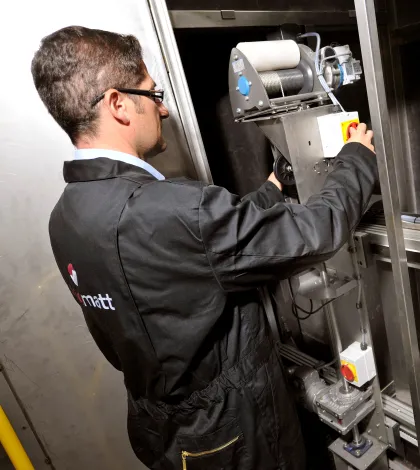
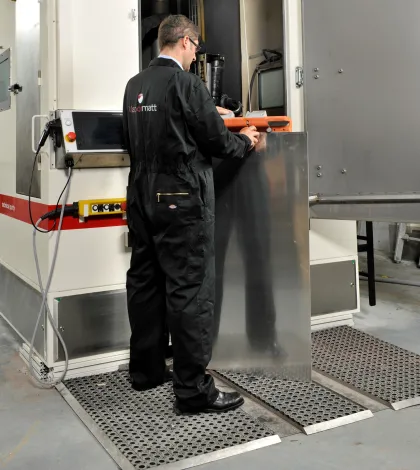
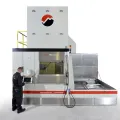
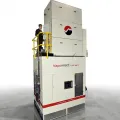
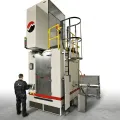
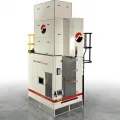
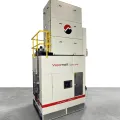
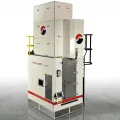
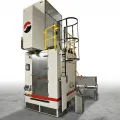
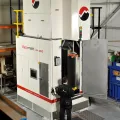
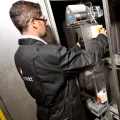
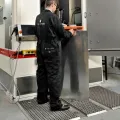
The Leopard Vertical is fully automatic and built for tall components such as fan blades. Servo-driven vertical and horizontal oscillation keeps nozzle distance and angle approximately constant as the guns traverse the component, with or without a turntable. The Leopard Horizontal is built for heavy and large-diameter components, taking up to 5,000kg (11,023lb) on a 1.85m (73") turntable. A powered trolley slides the turntable out to an external load station so a single operator can load at floor level, and an optional manual workstation allows touch-ups without unloading. Both configurations share the same process control architecture, are programmable with up to 8 axes of motion through the HMI, and are configured to fit your facility.
Process control and compliance
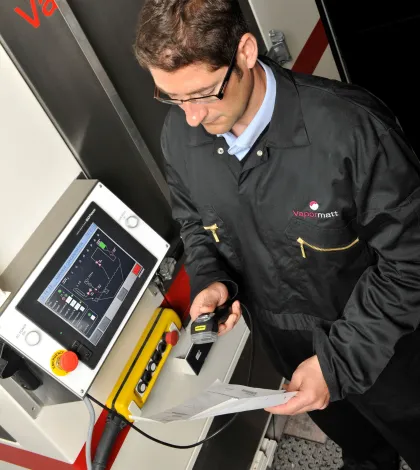
The Leopard continuously monitors slurry pressure, blast air pressure and airflow, and shuts down automatically within one second of any drift outside set limits, meeting the computer-monitored peening requirements of AMS 2432. The optional slurry concentration sensor adds closed-loop control of abrasive concentration, with watchdog limits that stop processing if concentration drifts outside set bounds. Every cycle runs from a stored recipe selected on the HMI, and an optional barcode scanner selects the correct recipe from the batch card. Vapormatt 4.0, fitted as standard to new machines, logs process parameters for every cycle for audit.
Why choose the Leopard
Vapormatt has built only wet blasting machines since 1978, and the Ashworth family’s work on the process goes back to the late 1940s, when Norman Ashworth developed wet blasting alongside Sir Frank Whittle’s jet engine work. Vapormatt machines are in use processing components to Rolls-Royce, GE and Pratt & Whitney specifications.
- Patented doughnut sump (EP1859902B1): eliminates the pit requirement entirely, placing the working envelope at floor level and removing civil installation cost and programme delay.
- Up to 8-axis programmable motion: maintains optimal nozzle angle and standoff across compound geometry, eliminating coverage gaps that cause non-conformances on complex components.
Lower running costs: vortex slurry pumps, continuous hydrocyclone filtration and optional MK9 blast guns, around 10% more efficient than the standard MK3 guns, reduce energy consumption, media usage and waste while meeting the environmental and operator safety standards aerospace facilities require.
Vapormatt has filed 12 wet blasting patents over four decades, covering nozzle design, slurry management, particle separation and machine architecture, including the doughnut sump fitted to every Leopard and the optional elutriation tower that keeps peening media in grade.
The Vapormatt Promise: the machine meets the agreed specification, or we make it right.
The bottom line
The Leopard is the large-format wet blasting machine for aerospace OEMs and MRO facilities processing components where process failure is not an option. Choose the Leopard Vertical for tall components up to 100kg (220lb), such as fan blades, and the Leopard Horizontal for heavy or large-diameter components up to 5,000kg (11,023lb), such as engine casings. For MRO teams whose components do not need the full Leopard envelope, see the Leopard Cub. For general production peening and cleaning of components up to 1,000kg (2,205lb), see the Cougar+. Facilities relying on fixed-configuration or manually loaded alternatives carry the compliance risk of coverage gaps and the operational cost of machines that cannot adapt as the component mix changes. The Leopard removes both.
Technical specifications
| Parameter | Leopard Vertical | Leopard Horizontal |
|---|---|---|
| Footprint (W × D × H) | 2,575 × 1,100 × 2,804 mm (102" × 43" × 110") | 7,000 × 4,000 × 4,000 mm (276" × 158" × 158") |
| Turntable diameter | 800 mm (32") | 1,850 mm (73") |
| Maximum component weight | 100 kg (220 lb) | 5,000 kg (11,023 lb) |
| Electrical supply | 400/480V, 3-phase, 50/60Hz, 63A | 400/480V, 3-phase, 50/60Hz, 63A |
| Process air | 6–7 bar (90–100 psi); 1.15 Nm³/min (40 SCFM) per gun at 10 mm nozzle | 6–7 bar (90–100 psi); 1.15 Nm³/min (40 SCFM) per gun at 10 mm nozzle |
| Cabinet construction | Welded stainless steel with abrasion-resistant lining | Welded stainless steel with abrasion-resistant lining |
| Configuration | Fully automatic; servo vertical and horizontal oscillation, with or without turntable | Automatic radial blasting, with optional manual workstation for touch-ups |
| Axes of motion | Up to 8, programmed via the HMI | Up to 8, programmed via the HMI |
| Loading | Low-level loading through a large access door; no pit | Powered trolley slides turntable out to an external load station; low-level loading, no pit |
| Turntable speed | 1–10 RPM, servo-driven (where fitted) | 1–10 RPM, servo-driven |
| Slurry pumps | 2 × 50mm (2") 5.5kW vortex pumps on swing-out mounts | 2 × 50mm (2") 5.5kW vortex pumps on swing-out mounts |
| Blast guns | MK3 guns with 10mm (0.4") boron carbide nozzles; MK9 guns, 12mm nozzles and micro nozzles optional | As Vertical |
| Process monitoring | Slurry pressure, blast air pressure and airflow standard; slurry concentration sensor, airflow monitoring, MES logging and barcode recipe selection optional | As Vertical |
| Noise level | Max 80 dBA | Max 80 dBA |
Full technical specifications are available in the downloadable Leopard machine brochure