Image

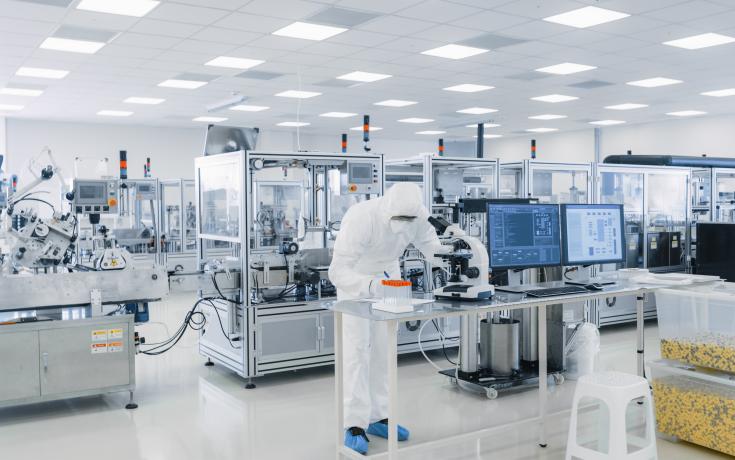
Sterilisation only works on surfaces it can reach. Weld marks, machining lines and uneven roughness leave peaks and crevices where bacteria and residue survive cleaning and sterilisation cycles. Wet blasting replaces them with a uniform, non-directional surface in the ideal roughness range for sterilisation, down to 0.4 µm Ra on stainless steel, so components clean and sterilise reliably, batch after batch.
In a single controlled pass, a slurry of water and fine abrasive removes weld scale, heat tint and machining marks and leaves a measurable surface roughness. Abrasive grade, pressure and dwell time set the Ra. Finer media at lower pressure gives the smoothest finish, ideal for sterilisation, while a more aggressive grade is used where heavy weld contamination must come off first. One machine can deliver both.
Talk to an applications engineer about your finishing for sterilisation requirements
The slurry stream combines water and abrasive into a single flow that simultaneously abrades the surface, flushes contamination, and moderates the energy of each particle. This produces a uniform, low-variance surface roughness across complex geometries including weld seams, internal corners, and tubular sections. The result is a surface that is both visually consistent and measurable against a specified surface roughness target.
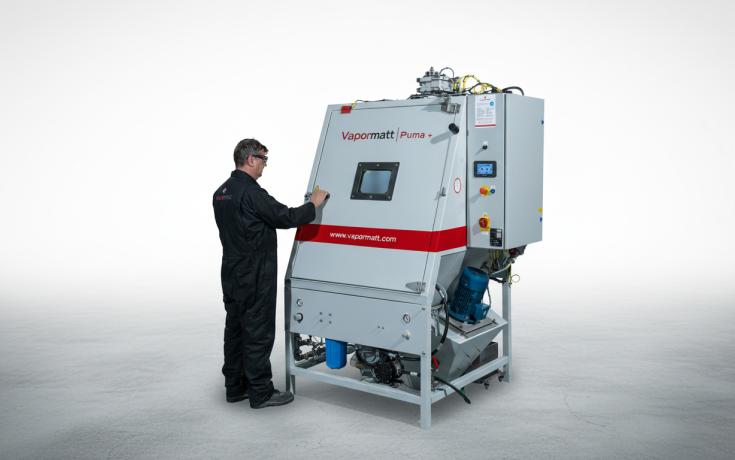
Typical setup: hygienic finish wet blasting
The lower and more uniform a surface’s roughness, the fewer peaks and troughs there are for bacteria to shelter in during cleaning and sterilisation. For product-contact surfaces, EHEDG guidance cites a maximum of 0.8 µm Ra. Wet blasting is set to hit your Ra target, not just to look clean. The figures below are indicative starting points from Vapormatt sample trials for you to qualify against your own specification. They are not guaranteed specifications.
| Component type | Typical size or weight | Process mode | Achievable outcome | Minimum control |
|---|---|---|---|---|
| Stainless steel tubular frame, medical trolley | Up to 1m x 0.5m | Manual | Weld discolouration removed, minimal change to existing surface finish | Basic manual machine |
| Stainless steel shower drain tray | 900mm x 150mm x 100mm | Automatic | Ra 0.4-1.5 µm achievable depending on abrasive and pressure selection; all machining and weld marks removed | Automatic component motion |
In sample trials on 900 × 150 mm stainless steel shower drain trays, aluminium oxide at 5.5 bar with four guns in simulated automatic mode processed 60 parts per hour and removed all machining and weld marks, giving 0.9–1.5 µm Ra across four processes. These settings were chosen to remove heavy marks quickly. As the table above shows, finer media at lower pressure takes the finish down to 0.4 µm Ra, well within the EHEDG 0.8 µm guideline for surfaces that must be sterilised.
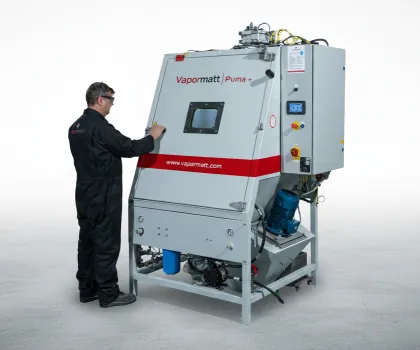
Iskra PIO, a Slovenian pharmaceutical machinery manufacturer, partnered with Vapormatt to adopt wet blasting using the Puma and Leopard Sump machines, replacing manual polishing and brushing to achieve faster, more consistent hygienic stainless steel surface finishes below 0.8μm Ra.
Finishing surgical or dental instruments for autoclave sterilisation? See our medical and dental instrument finishing page.
Sterilisation relies on steam, heat or chemicals reaching every part of a surface. Rough or uneven surfaces have peaks, troughs, scratches and weld marks where bacteria and residue can shelter, form biofilms and survive cleaning and sterilisation cycles. A lower, more uniform roughness leaves fewer of these hiding places, so cleaning removes more and sterilisation is more reliable. Wet blasting doesn’t sterilise components itself. It creates the controlled surface roughness that makes sterilisation work.
For product-contact surfaces in food and pharmaceutical equipment, EHEDG guidance cites a maximum of 0.8 µm Ra, and some medical and pharmaceutical specifications set lower limits. Wet blasting is set to your target. Finer media at lower pressure gives the smoothest finishes, down to 0.4 µm Ra on stainless steel in Vapormatt trials, while more aggressive settings for heavy weld contamination give a higher Ra. We recommend a sample trial to confirm the recipe against your specification.
Yes. Glass bead and aluminium oxide are non-ferrous, so wet blasting doesn’t leave free iron on the surface, and stainless steel components can be passivated afterwards if your specification requires it.
At the pressures used for hygienic finishing, material removal is minimal. The process removes surface contamination and levels the finish rather than cutting into the substrate. For close-tolerance components, we recommend a sample processing trial before committing to production parameters.
Visual inspection does not confirm Ra. Surfaces that look clean can still carry peaks and troughs that trap bacteria and resist sterilisation. The hygiene standards for stainless steel in medical and food environments specify Ra values in the 0.25 to 0.6 µm range; wet blasting gives you a process you can measure and repeat to that target.
Ra is measured with a contact profilometer before and after processing. In Vapormatt sample processing trials, process variance across four measurement points on a stainless steel tray was a standard deviation of 0.07 µm Ra at the lowest-variance setting. Consistent abrasive grade, pressure, and dwell time are the controls; all three are lockable on Vapormatt equipment.
Yes, with the right abrasive selection. A mix of aluminium oxide and glass beads removes weld scale and produces a consistent finish in one operation. Where weld contamination is heavy, a more aggressive abrasive grade may be required; this shifts the Ra outcome upward, so the process recipe needs to be confirmed against your finish specification.
No. Entry-level wet blasting machines for this application require only basic process control. The recipe is set and locked; the operator loads and unloads components. More complex geometries or tighter Ra tolerances may warrant a step up in machine capability, but the majority of hygienic finishing work on standard stainless fabrications does not require specialist intervention.